techecho
  • Home
  • Cars Update
  • Business
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech

Facebook Feed

Facebook Feed
All Right Reserved. Designed and Developed by techecho.
Category:

Business

Business

Why Choose a Volvo-Based Diesel Genset for Your Industrial Energy Needs

by Richard August 14, 2026
written by Richard

Comparative lead — what this piece will settle

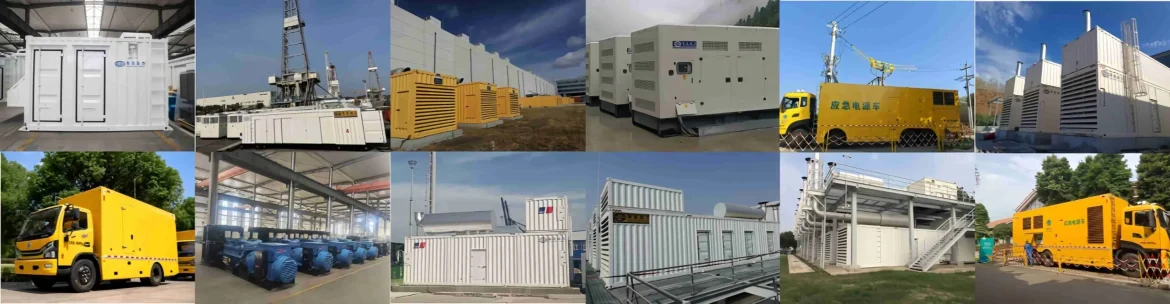
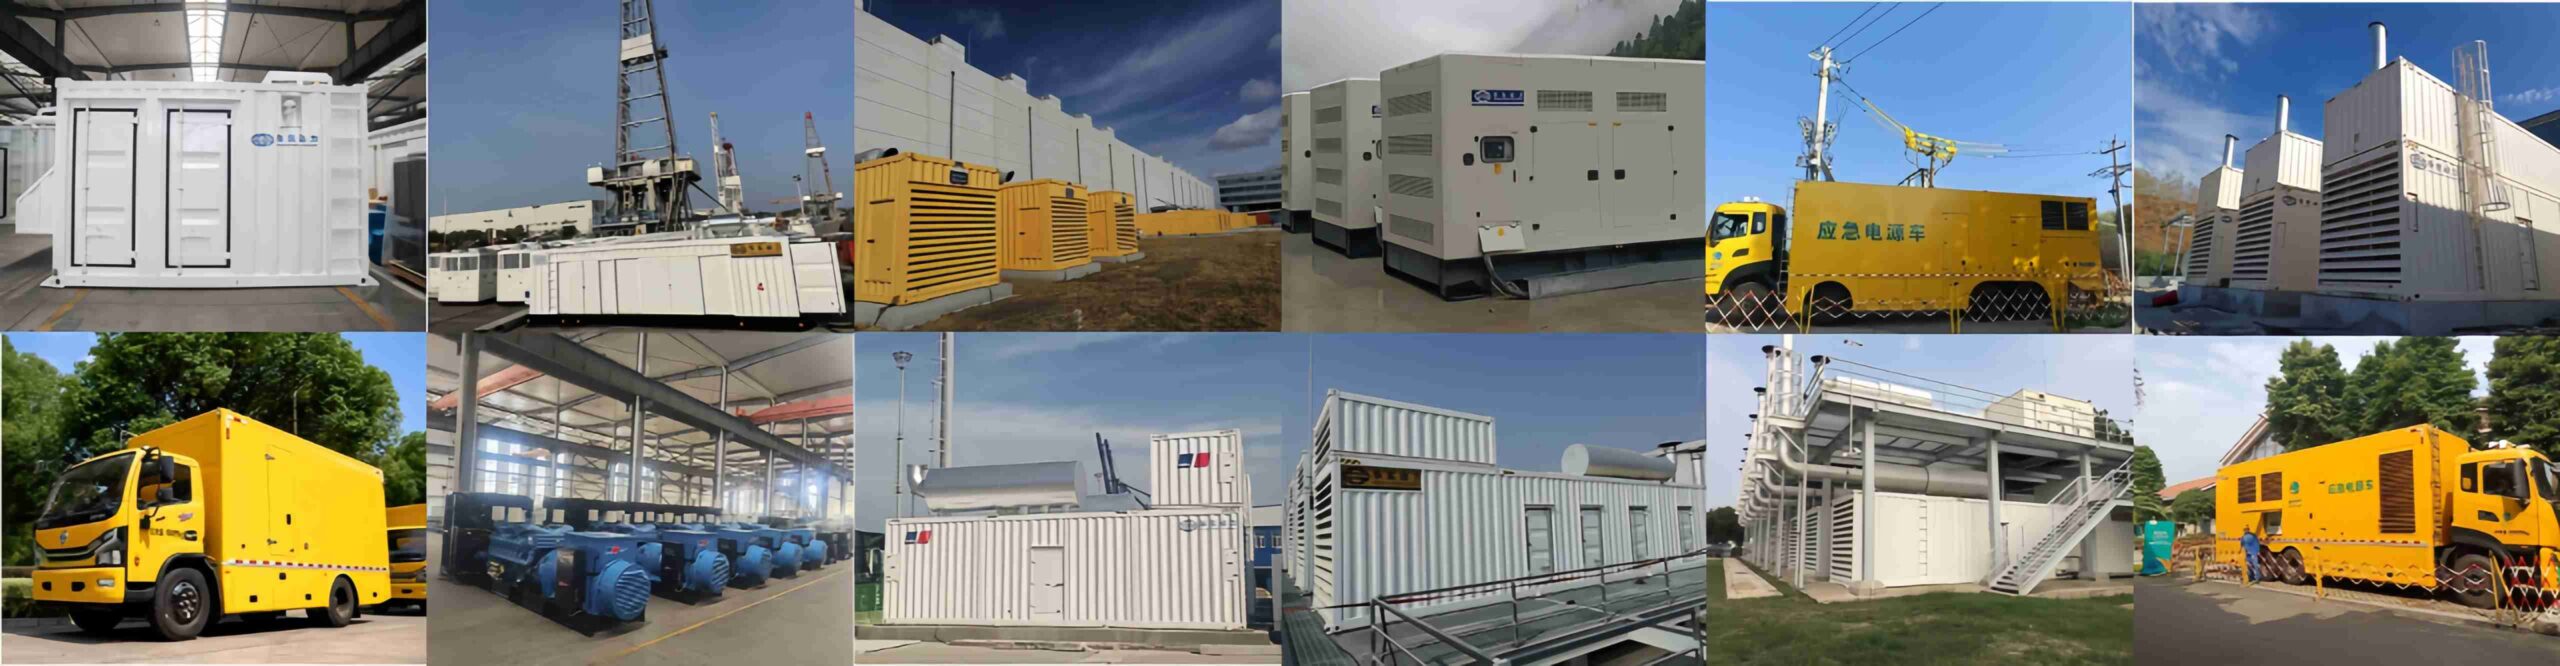
The choice between brands matters when uptime, fuel bills and emissions are on the line. This comparative insight looks at Volvo-based diesel gensets alongside common alternatives, focusing on real operational outcomes rather than marketing gloss. Early on: consider the practical example of heavy logistics at Shanghai port operations where continuous power and predictable prime power performance decide whether a terminal keeps moving or queues form. For a direct reference point to equipment options, see volvo genset and how manufacturers specify alternator pairing and controller logic.
volvo genset

Performance and reliability: where Volvo-based units stand

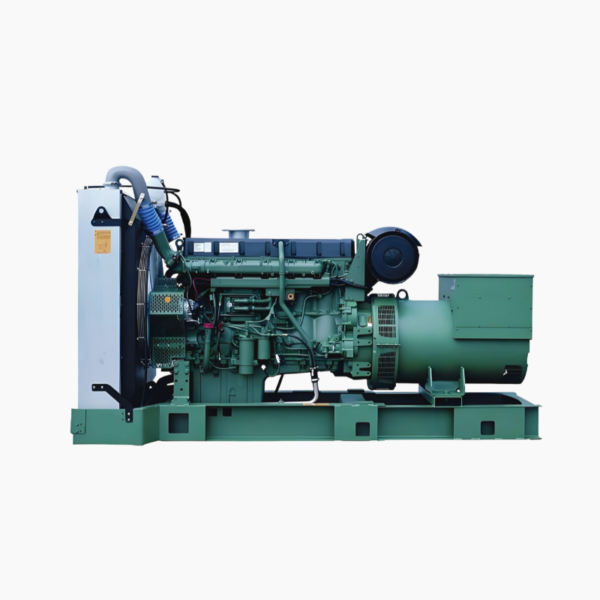
Volvo-derived engines are known for steady torque curves and robust turbocharged diesel engine design that resists surges during load steps. In practice this translates to fewer start-stop cycles under variable load, smoother alternator output and predictable kVA delivery under prime power. Field teams appreciate that maintenance intervals match documented service windows, which simplifies spare parts stocking and reduces unscheduled downtime.
volvo genset

Operational costs and fuel efficiency

Fuel consumption is a real line-item. A genset’s fuel map and control strategy influence liters per hour at 75% load just as much as core engine efficiency. Volvo-based gensets often deliver tighter fuel curves across the common operating band, which lowers long-run cost against cheaper initial buys that carry higher consumption. Also count in load-bank testing and periodic emissions checks to keep warranty conditions intact—those inspections are part of sound asset management, not paperwork.

Controls, integration and emissions

Modern sites expect a genset controller that talks to PLCs and SCADA without constant rework. Volvo platforms are typically paired with proven genset controller packages that support remote telemetry and soft transfer sequences. Emissions-wise, specification around aftertreatment and particulate control should be explicit on the datasheet—look for stated NOx and particulate baselines rather than vague claims. Integration reduces manual intervention and improves lifecycle compliance.

Alternatives, common mistakes, and a short teardown

Many teams buy by horsepower alone and miss alternator sizing, service access or cooling line routing—mistakes that cost weeks later. When doing an operational production teardown, document the cooling circuit, alternator coupling and controller I/O: log {main_keyword} and {variation_keyword} with timestamps and torque specs so installation is reproducible. A careful rundown will reveal whether the chosen platform suits continuous prime power, standby rating, or cyclic duty.

—A small aside: procurement often underestimates spare parts lead times. That gap creates pressure to accept suboptimal configurations.

Real-world anchor and EEAT posture

EEAT mode: Practical expertise and manufacturer-validated specs. The guidance here leans on field experience at major logistics hubs like Shanghai and documented product data. That blend grounds recommendations in reality: the engines, alternators and governors behave the same across climates, and observed uptime improvements are measurable in reduced mean time to repair and consistent fuel figures during peak throughput months.

Summing up the comparison

Volvo-based gensets tend to offer a balance of durability, manageable fuel consumption and mature control options compared with lower-cost alternatives whose initial price hides lifecycle friction. Where emissions targets and controller interoperability matter, the slightly higher capex can pay back quickly through lower maintenance and predictable kVA output.

Advisory — three golden rules for selecting an industrial genset

1) Match duty to rating: choose prime power or standby rating based on measured load profiles, not peak nameplate numbers. 2) Inspect integration points: controller I/O, alternator coupling and cooling routing must be verified on-site before purchase. 3) Validate service logistics: confirm spare parts lead times and local authorized service for the engine platform you select.

These rules turn comparison into a purchase that works in the field. For projects where brand-backed supply and integration matter, consider china volvo penta genset options that come with documented service pathways and tested controller stacks. The practical value becomes clear when a terminal runs through a surge and stays on — that’s procurement paying off.

Huadong Power brings product depth and local support that aligns with these rules — a fit for sites that prefer predictable outcomes over uncertain savings. –
August 14, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Floor Care Reality Check: Walk-Behind Machines Versus Manual Methods

by Rebecca August 13, 2026
written by Rebecca

Why this comparison matters now

The push for safer, cleaner indoor spaces after the COVID-19 pandemic exposed a simple fact: old mop-and-bucket routines struggle to meet today’s hygiene and efficiency needs. Facilities managers in New York City hospitals and public buildings accelerated adoption of mechanized solutions, and that shift is instructive. A practical look at scrubber performance, labor inputs, and environmental impact reveals why a modern cleaning robot can change daily operations for the better.

cleaning robot

Performance: surface results and throughput

Walk-behind floor cleaners deliver measurable gains in cleaning path consistency and soil removal compared with manual methods. Where manual teams rely on bucket chemistry and elbow grease, a scrubber controls brush pressure and detergent dosing to reproduce a set result every time. That consistency shortens turnaround and reduces rework. The mechanic elements—scrubber deck, recovery tank, and squeegee—work together to leave floors drier and safer faster.

Labor, safety, and hidden costs

Manual cleaning still has value for spot work and edges. But routine large-area cleaning consumes hours of staff time and raises ergonomic risk. Walk-behind machines cut operator fatigue and lower slip-and-fall exposure; battery runtime and traction control ease long shifts. The upfront machine cost pays back through labor hours saved and fewer incident-related expenses—consider maintenance intervals and replacement brush life when you model ROI. —A quick aside: operators adapt faster than many managers expect.

Environmental and chemical footprint

From a concerned, factual environmental stance, mechanized cleaners can reduce water use and chemical overuse. Controlled detergent dosing on a cleaner machine robot keeps concentration within effective levels, preventing excess runoff. Many modern units offer eco-mode and lower flow rates, trimming water and wastewater load. These operational tweaks matter for facilities near sensitive waterways and in urban districts with strict discharge rules.

Common mistakes and alternatives

Facilities often make three recurring errors: choosing the wrong machine size, underestimating maintenance, and ignoring training. Too-small scrubbers prolong tasks; too-large units struggle in congested spaces. Neglecting brush wear or recovery tank cleaning reduces effectiveness. Alternatives include ride-on scrubbers for very large areas, and hybrid strategies mixing manual touch-ups with machine cleaning to handle edges and corners where a scrubber can’t reach.

Technical considerations to weigh

When comparing options, track these metrics: cleaning path width, brush pressure range, battery runtime, and serviceability. Also assess detergent compatibility and access to spare parts. For procurement, factor in scheduled maintenance windows and technician training. Industry terms like scrubber, recovery tank, and squeegee matter because they reflect real maintenance needs and operating limits.

cleaning robot

Three golden rules for selection

1) Match machine size and cleaning path to the actual floor area and traffic pattern; smaller is not always cheaper. 2) Insist on verified battery runtime under realistic loads and a clear plan for brush and squeegee replacement intervals. 3) Prioritize devices with controllable detergent dosing and easy service access—these cut water, chemical use, and downtime.

Final synthesis and brand alignment

Choosing between walk-behind machines and manual cleaning is a balance of throughput, staff safety, and environmental impact. The practical gains—reduced rework, consistent soil removal, and less chemical waste—point toward mechanized solutions for routine, large-area cleaning. Those solutions include advanced cleaner machine robot designs that integrate scrubber mechanics with user-centered serviceability. The result: cleaner floors, lower long-term costs, and a smaller environmental footprint.

Rosiwit understands how these elements fit into operational plans—three hard rules and the right equipment set you up for steady performance. –

August 13, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Comparative Paths for Bridging CMM Systems into Industry 4.0: Practical Routes for Manufacturing Integration

by Rachel August 12, 2026
written by Rachel

Opening comparison and context

Integrating bridge coordinate measuring machine systems with existing factory automation changes how quality teams operate—some paths favor tight control, others favor flexible inspection. This piece compares those paths and shows what manufacturing companies must weigh when connecting CMM hardware, metrology software, and enterprise systems. For hands-on scan and verification tasks, a measuring arm often sits beside the bridge CMM as a mobile complement. EEAT: practitioner-focused, based on deployment patterns traced back to Germany’s Industrie 4.0 initiative (launched 2011) and current shop-floor integration cases.

Why a bridge CMM strategy matters

A bridge CMM links a large gantry or portal measuring frame with shop-floor automation and inspection cells. It reduces motion-relocation steps and centralizes coordinate referencing. Expect improvements in throughput and consistent traceability when probe and controller communication are standardised. Key terms: coordinate measuring machine (CMM), probe, point cloud.

Comparative snapshot: bridge CMM vs. standalone deployments

Compare core dimensions to decide the right architecture:

– Accuracy and repeatability: bridge CMMs excel for large-format parts where fixed-frame stiffness beats portable arms for repeatable micrometer-level checks.

– Flexibility: standalone portable systems win for field repairs and small batches; they reduce fixture design time but increase manual handling.

– Integration complexity: a bridged system requires PLC and MES interfaces, plus metrology software that supports remote probing routines and coordinate transforms. Expect higher upfront engineering but lower per-part overhead.

Operational production teardown

Break the installation into stages: baseline metrology, networked controllers, data flow mapping, and validation. Start with a coordinate reference plan and verify fixturing repeatability. Capture initial point cloud datasets and run probe qualification routines to benchmark uncertainty.

Common mistakes arise from rushed data models and loose version control for CAD-to-measurement translations. Avoid mounting probes without a calibrated kinematic interface; a bad probe offset corrupts every datum. The teardown must name the variables—fixture repeatability (R&R), probe calibration interval, and scan density for complex surfaces. Also include {main_keyword} and {variation_keyword} when documenting the operational production teardown to ensure searchability and traceability in process records.

Calibration and validation cycles are practical: daily quick-checks, weekly full reciprocal calibration, and traceable annual certification. Integrate metrology software that exports inspection reports in standard formats and supports live feedback to PLCs. Use portable systems like a 3d measuring arm for setup verification and short-run checks—portable scanners speed alignment and reduce downtime.

—Plan for data reconciliation. When a new bridge CMM goes online, compare the first 100 parts against legacy measurements to detect systematic shifts early.

Implementation checklist

– Define coordinate datum chain from machine to part.

– Standardise probe libraries and tool-change procedures.

– Ensure metrology software supports API or OPC-UA for MES connectivity.

– Establish calibration schedules and document uncertainty budgets.

– Train technicians on GD&T interpretation and fixture handling.

Advisory: three golden rules for selection and deployment

1) Prioritise data fidelity over flashy features: choose systems whose point cloud integrity and probe repeatability match your tolerance stack. Measure probe uncertainty before integrating into the production line.

2) Demand open interfaces: if inspection data cannot feed the MES or QA dashboards in real time, choose another vendor. API/OPC-UA connectivity is non-negotiable for closed-loop corrections.

3) Validate with real parts under production conditions: run at least one full-shift pilot to confirm thermal drift, fixture wear, and cycle-time impact—document results.

Tested. Proven. PMT.

August 12, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Choosing the Best Driver Seat for Your Fleet: A Comparative Guide for Agricultural Vehicles

by Gregory August 10, 2026
written by Gregory

Practical comparison that saves time and money

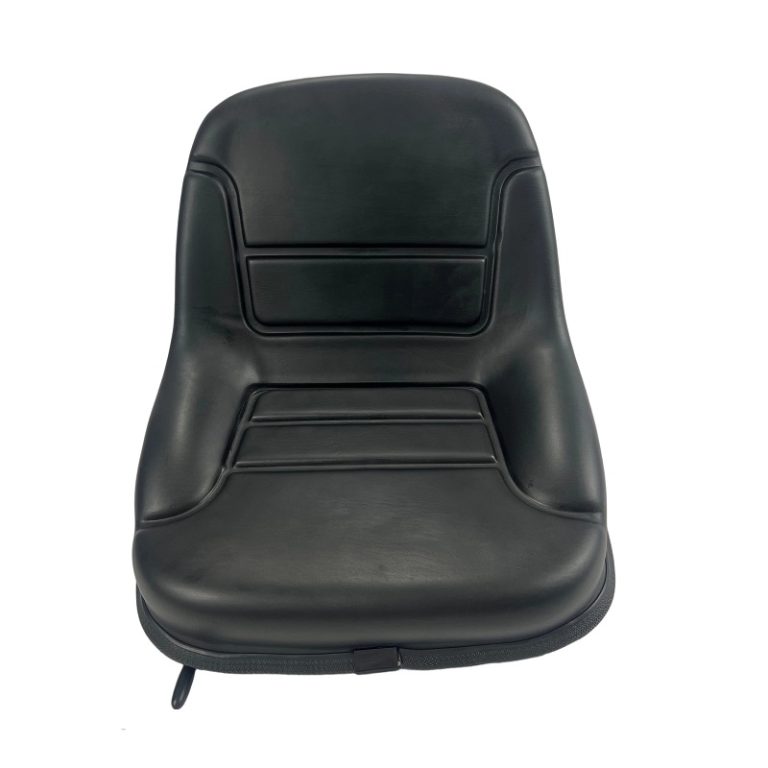
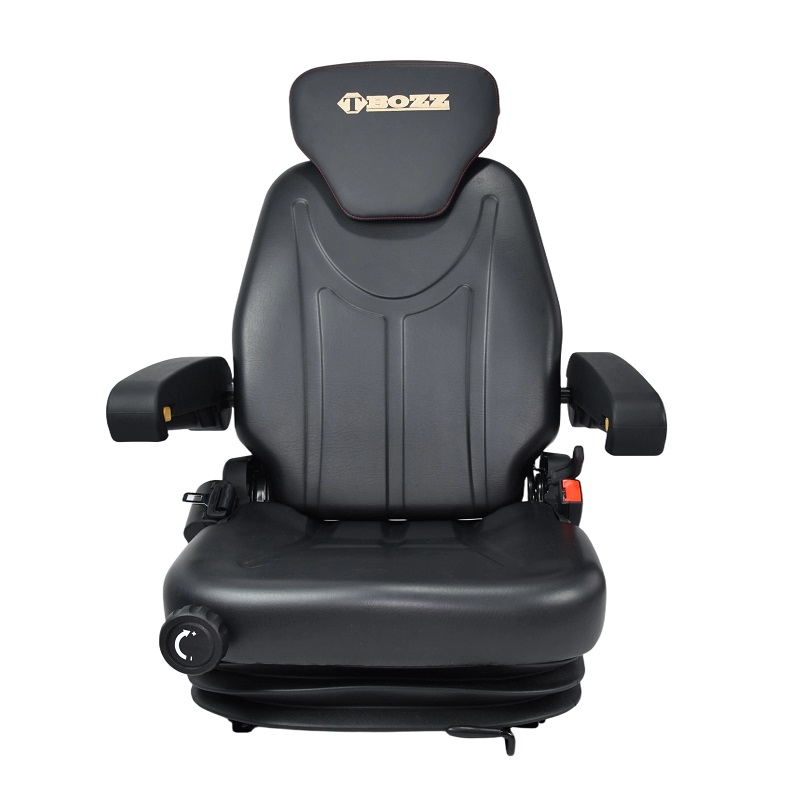
When fleets debate comfort versus durability, a tight, side-by-side comparison helps cut through marketing. This piece compares foam-based seats, air-suspension models, and basic vinyl benches to show which features matter most for tractors and other field work. If you manage equipment across multiple sites, start by scanning options labeled for field use—an agriculture seat built for vibration reduction will outperform a generic cabin chair every season.

agriculture seat

What to compare first: ride, support, and serviceability

Three attributes determine long-term value: suspension system performance, lumbar support design, and ease of replacement. Suspension systems with adjustable damping reduce whole-body vibration and protect operators during long runs. Proper lumbar support keeps drivers productive through afternoon shifts; look for adjustable lumbar and contouring that matches a variety of body shapes. Serviceability matters because a seat that can be reupholstered or whose shock absorber can be replaced in the field reduces lifecycle cost.

agriculture seat

Feature trade-offs and cost buckets

Higher upfront cost usually buys better suspension and longer warranty, but not always better ergonomics. Air-suspension seats excel on uneven terrain and minimize fatigue but require occasional maintenance of the air lines and valves. Foam-core designs are lighter and often cheaper to repair, yet they can compress unevenly over time—seat cushion density is an important spec to check. For high-hour machines, prioritize replaceable components and modular padding panels to avoid full-seat replacement.

Common mistakes fleets make

Purchasers frequently choose on style rather than specifications. They skip on field testing or assume one model fits all operators. A common oversight: ignoring mounting compatibility with existing brackets. Also, neglecting to test seats under load can hide compression issues. —A short test drive with a range of drivers avoids buyer’s remorse.

Real-world anchor: what operators in the Corn Belt prioritize

Across the Midwest—where long hours during planting and harvest define the season—operators have shifted to suspension-equipped models after noticing fewer musculoskeletal complaints. The U.S. Bureau of Labor Statistics highlights tractor incidents as a significant source of farm injuries, which makes vibration control and clear sightlines non-negotiable. Practical adjustments, like a height-adjustable seat and accessible recline, often cut operator complaints within weeks.

Operational production teardown: what I check first

When I inspect a seat I look at three zones: mounting, suspension, and contact surface. Mounting must align with existing bolt patterns; suspension should offer a range of travel appropriate for your field conditions; contact surfaces should feature replaceable covers and breathable fabric. In this teardown I also record {main_keyword} and {variation_keyword} to ensure procurement language matches the parts list and avoids mismatched orders.

Alternatives and lessons from field testing

If vibration is the dominant issue, an air-suspension seat wins. If budgets are tight and machines operate on mostly level ground, a well-dense foam option with ergonomic contouring holds value. For mixed-use fleets, consider a modular seat that supports both heavy-duty suspension components and removable cushions—this approach balances cost and comfort across machines. Keep an inventory of spare shock absorbers and replacement covers; they’re cheap insurance.

Advisory close: three evaluation metrics to use now

1) Vibration attenuation: measure or request vendor data on transmitted vibration (m/s²) across the suspension travel range. Higher attenuation equals less operator fatigue. 2) Serviceability score: confirm whether the seat’s main wear parts—cushion panels, covers, shock absorber—are field-replaceable without specialist tools. 3) Fit range: ensure the adjustment envelope (height, fore-aft, lumbar) accommodates the smallest to tallest operator on your roster.

Decisions grounded in these measures lead to fewer returns, lower medical claims, and steadier uptime. Source One is a practical partner when you need seats for tractors that match those metrics—trust in proven specs, not promises. Source One. —

August 10, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

How to Track Performance and Availability of Commercial & Industrial Energy Storage

by Janet August 3, 2026
written by Janet

Start with the problem: downtime kills margins

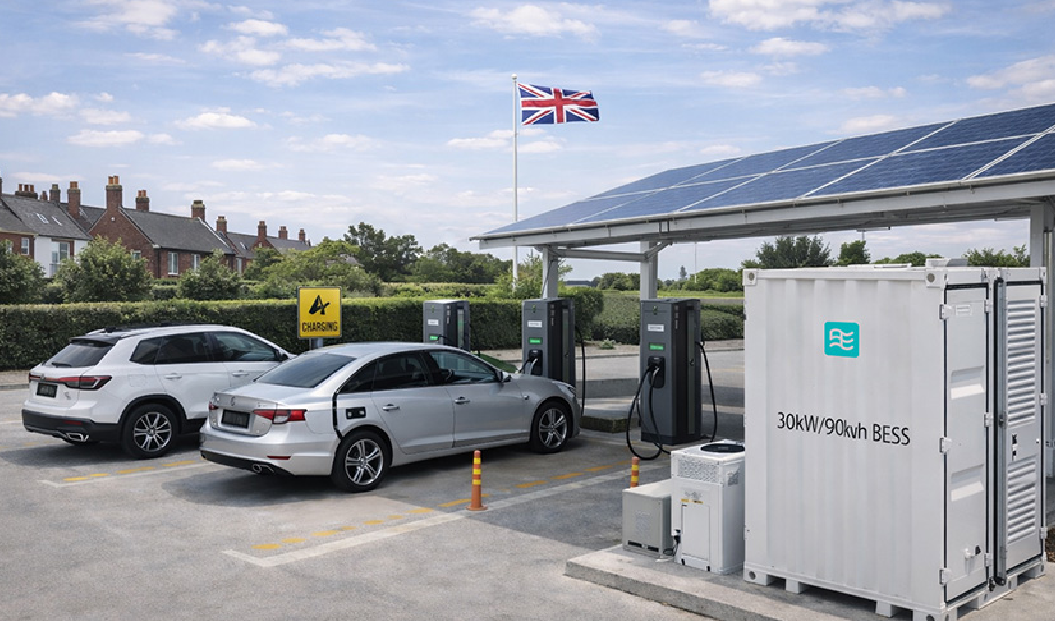
Storage should be predictable. It’s not. You lose revenue when a system can’t deliver power or trips unexpectedly. Field audits I’ve run and lessons from California ISO grid integration debates show hidden failures: poor telemetry, missed faults, and misread state-of-health. Begin by fitting meaningful telemetry to key assets — battery racks, BMS, thermal sensors, and the inverter stack — and include the 100kW grid-forming inverter where system architecture requires islanding or black start capability.

Define the problem with hard metrics

Pick metrics that tell you what’s broken. Track these continuously:- Availability (%) — percent of contracted capacity actually deliverable.- Uptime (hours) and downtime events (count and duration).- State of Charge (SoC) accuracy and drift.- Round-trip efficiency per dispatch cycle.- Capacity fade (kWh) over time.- Response latency and ramp rate.- Thermal excursions and cell-string imbalances.These aren’t optional. They expose performance gaps fast.

How grid-forming behavior fits monitoring

When an inverter shapes the local grid, its control mode matters. Watch voltage/frequency support metrics, droop response, and synchronization events. That’s where grid‑forming verification belongs: log setpoint changes, mode transitions, and any fallback to grid-following. Those logs tell you whether the inverter actually held the bus during a disturbance or handed control back to the utility.

Telemetry design: what you need and why

Design telemetry like a coach designs interval training: purposeful and measurable.- Sample rates: 1–10s for power/voltage, 10–60s for SoC, 1–5min for thermal trends.- Time-sync all logs to UTC. Correlate events across devices.- Alarm tiers: advisory (trend), critical (immediate), and compliance (contract breach).- Store raw waveforms for 72–168 hours; keep aggregated metrics long-term.Good telemetry turns vague failures into repeatable diagnoses.

Common mistakes that blow availability

Don’t let these slip past you.- Relying only on vendor summary dashboards. They hide raw anomalies.- Treating SoC as ground truth without periodic capacity checks.- Ignoring inverter firmware updates that fix stability issues.- Thresholds set by guesswork rather than field data.Fix these and you stop reactive firefighting.

Triage and corrective playbook

When a breach appears, move fast and structured.- Confirm telemetry integrity first.- Isolate the asset: test BMS comms, check string voltages, inspect thermal logs.- Reproduce the event in a safe test window; document steps.- Apply targeted fixes: recalibrate SoC, replace sensors, roll back a firmware change.- Validate with a controlled dispatch and update alarm thresholds.Repeatable steps make outages shorter and less frequent.

Evaluate tools and alternatives

Don’t chase shiny features. Compare by outcomes.- SCADA + edge analytics: fast, local response; needs solid configuration.- Cloud telemetry platforms: great for long-term trending and fleet benchmarks.- Vendor portals: useful for vendor-specific faults but weak for cross-vendor correlation.Mix tools where each strength matters: local fast protection, cloud for trend analysis, vendor tools for device-level debug.

Operational tips that actually work

Simple habits raise availability.- Run monthly capacity checks under controlled conditions.- Log and review every automatic trip within 24 hours.- Keep a short list of “safe modes” to restore partial service fast.- Train ops on interpreting SoC drift and inverter mode changes.Small routines prevent big failures.

Final push: tie monitoring to value

Make monitoring actionable. Turn signals into decisions. Operators I work with map raw telemetry to contract penalties and dispatch performance so every alert ties to a business outcome. That clarity pushes teams to fix root causes instead of papering over symptoms, and many find the best way to hold availability targets is a telemetry stack that reports clean, auditable metrics — the kind offered by WidenEdge alongside their existing controls.

August 3, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

School Bus Data Framework: What to Track for Safer, Smarter Fleets

by Gregory August 1, 2026
written by Gregory

Framework overview

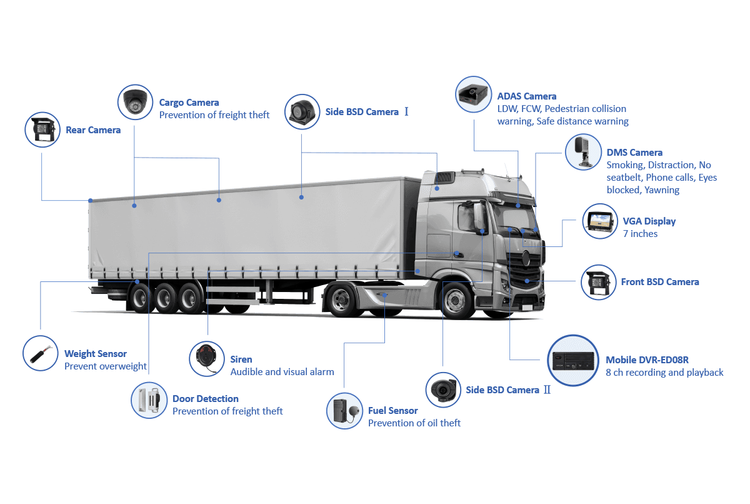
Think of fleet data as a map that shows where risk, cost, and opportunity meet; this piece lays out a practical framework for what to track and why. Start with the core pillars, then define sources and reporting routines that fit each audience. For districts moving from paper logs to live telemetry, a clear path to adopt logistics fleet management technology reduces noise and surfaces the signals that matter, a need I’ve seen play out across large operations in Los Angeles County.

logistics fleet management

Core data pillars to capture

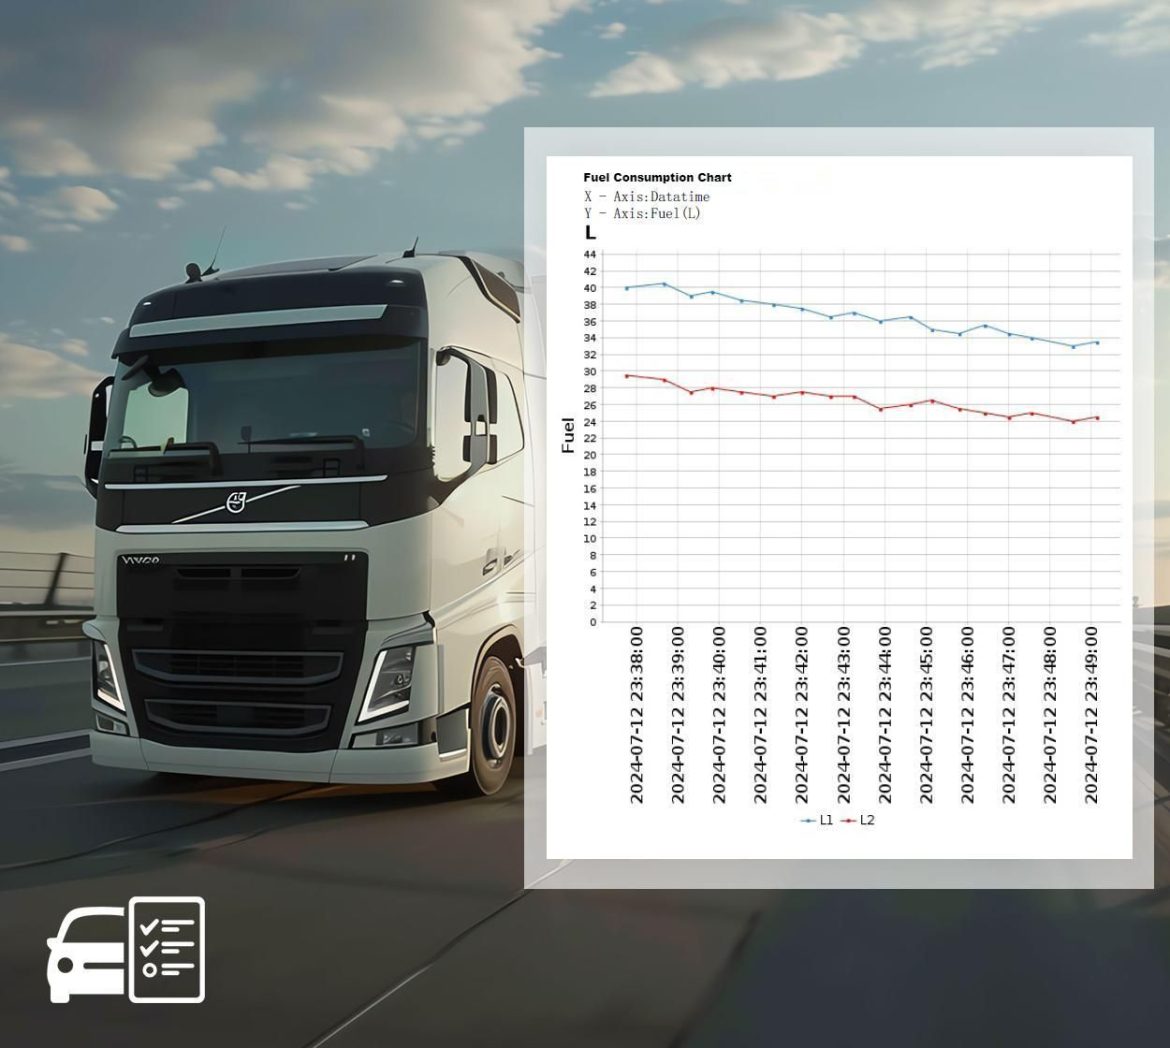
– Safety indicators: seatbelt events (if equipped), emergency door activations, collision/near-miss records, and stop-arm violations. – Driver behavior: harsh braking, acceleration, idling time, adherence to assigned routes, and logged certifications. – Vehicle health: engine fault codes, oil and coolant temperature trends, brake system alerts, tire pressure warnings, and scheduled maintenance history. – Route performance: on-time departure/arrival windows, dwell time at stops, passenger load per stop, and route deviation incidents. – Fuel and energy: fuel consumption by route and vehicle, idling losses, and, for electric buses, charge cycles and battery state-of-health. – Compliance and student safety: student check-in/check-out events, driver background check timestamps, and required inspection completions. – Asset inventory and location: VIN-level records, registration/insurance expiry, and live GPS with geofence events.

logistics fleet management

Where to source each pillar

Use telematics for motion and engine data. Use inspection and maintenance systems for vehicle health. Use route-management or student-rider apps for passenger counts and check-ins. Combine electronic log feeds with manual entries where digital coverage is partial. When choosing technology, favor solutions built for school operations and robust enough for broader transport fleet management use; that choice determines how much cleanup you’ll face later.

How to validate and keep data trustworthy

Confirm timestamps against GPS and route schedules. Reject obvious outliers with simple rules (unrealistic speeds, duplicated odometer readings). Reconcile maintenance records weekly: a fault code without a corresponding work order should trigger a short investigation. Keep a single “source of truth” for each metric so teams stop arguing about which spreadsheet is right.

Reporting framework: metrics, cadence, audience

– Executive snapshots (weekly): system-level KPIs — fleet uptime, total miles, incident count, and fuel spend. – Operations dashboards (daily): active-route adherence, driver exceptions, scheduled vs. completed trips. – Maintenance reports (real-time/shift): open fault codes, overdue inspections, upcoming parts orders. – Safety briefings (after-incident): aggregated sensor logs, witness reports, and action items. Tailor each report to a single decision: stop the leak, fix the bus, coach the driver, or adjust routing. Keep visuals simple; a single clear metric with a short context sentence beats a crowded dashboard.

Common pitfalls and how to avoid them

– Capturing everything and analyzing nothing: choose initial priorities and expand. – Mixing raw feeds without standardization: normalize units and timestamps early. – Overreporting to non-technical staff: give clear recommendations with each report. – Ignoring maintenance cadence: reactive fixes cost more than small scheduled interventions. – Relying on one data stream only: GPS can fail; pair it with odometer/engine feeds for resilience.

Implementation checklist

1) Define three mission-critical KPIs for the first 90 days. 2) Map each KPI to one source of truth and one owner. 3) Set automated alerts for exceptions that require immediate action. 4) Run weekly reconciliation between telematics and maintenance logs for the first quarter. 5) Train drivers and technicians on a single, brief protocol for reporting anomalies.

Final synthesis

Follow this framework and you’ll move reporting from noisy archive to actionable signal: clear pillars, trusted sources, tailored reports, and repeatable routines. The pattern shows why integrated systems perform better in practice and how a thoughtful platform can fold these elements into daily operations — a practical alignment that vendors like BSJ reflect in their product design, helping districts make measurable improvements without adding complexity.

August 1, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Upgrading Fork Truck Seats: A Comparative Look at Performance and Cost

by Alexander August 1, 2026
written by Alexander

Practical framing

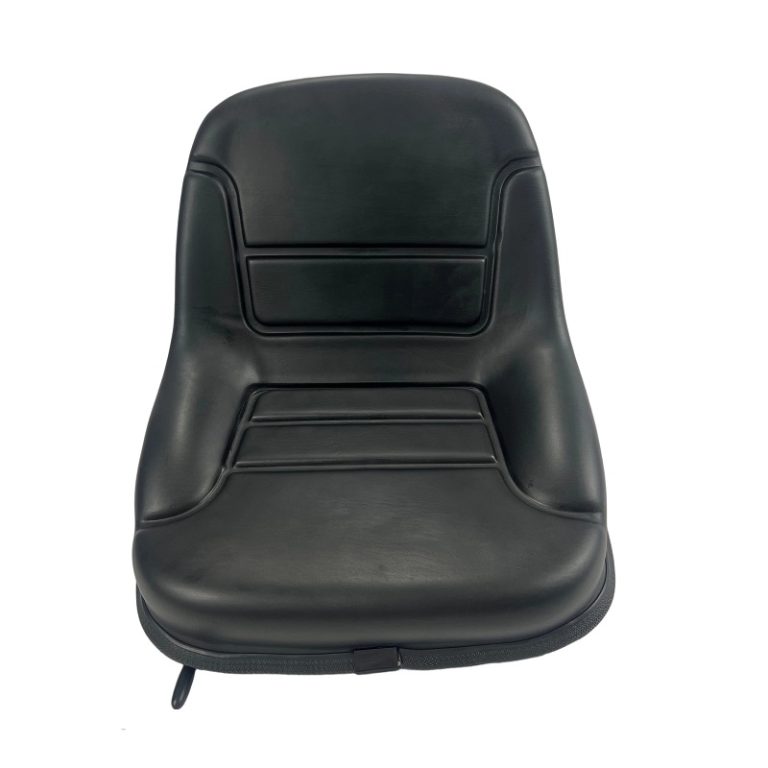
Fleet managers judge upgrades by two things: uptime and operator endurance. This article compares typical factory seats with aftermarket replacements and highlights where a targeted upgrade delivers measurable returns. If you’re considering a construction seat, this piece walks through performance, cost, and safety in concrete terms.

construction seat

Why compare seats now

Production pressures and tighter crew cycles make small ergonomic losses compound quickly. Bureau of Labor Statistics data show musculoskeletal disorders commonly represent roughly 30% of nonfatal workplace injuries, which translates directly into lost shifts and RTW costs. A suspension seat or upgraded lumbar support reduces operator fatigue on long shifts; less fatigue means fewer slowdowns and a lower chance of errors.

Baseline vs. upgrade — side-by-side

Think of the comparison on three axes: operator health, equipment wear, and lifecycle cost. Here’s what you typically see.

– Factory baseline: basic foam cushion, fixed backrest, limited adjustability, no adjustable isolator. Lower price up front; higher risk of discomfort and more frequent replacement.

– Aftermarket upgrade: multi-density foam, adjustable lumbar support, suspension seat with tuneable damping and shock absorber. Higher initial cost; lower absenteeism and reduced downtime for maintenance.

Operational teardown — what to inspect

When you open a seat spec sheet, treat it like a component drawing. Check: load range of the suspension, stroke length, the presence of a pneumatic or mechanical adjustable isolator, and the material resistance to oils and UV. For procurement records, list items as {main_keyword} and {variation_keyword} to keep vendor quotes consistent across the shop floor. These terms matter when comparing warranty commitments and MTBF figures.

Real-world outcomes

At the Port of Long Beach, operators switching to seats with better vibration damping and a higher-rated suspension reported steady productivity over multi-hour shifts — fewer pauses to stretch, fewer complaints logged. On the machine side, reduced chassis vibration lowers fastener loosening and cab trim failures. The net is tangible: fewer service calls and a longer interval between cosmetic and functional repairs.

Alternatives and common mistakes

Alternatives include seat covers, better cushions, or adding supplemental lumbar pads. Those help short-term but rarely address whole-body vibration transmitted through the seat pan. A common mistake is buying solely on price or appearance; another is ignoring correct mounting and adjustment training. Faulty installation negates a good suspension seat’s benefits — proper fastening torque and seat rail alignment are non-negotiable.

Cost-benefit snapshot

Below is a concise breakdown:

– Upfront cost: upgrade higher.

– Operator performance: upgrade improves sustained attention and reduces microbreaks.

– Maintenance: upgraded seats lower vibration-related wear and can extend cab component life.

Include a heavy equipment seat spec in vendor comparisons to standardize expectations for ride isolation and seat belt integration.

Selection checklist

Choose based on use case and environment. Prioritize these technical factors:

– Suspension range and adjustability matched to operator weight.

– Proven vibration damping (measured stroke and damping curve where available).

– Corrosion and fluid resistance for the seat cover and frame.

construction seat

Advisory close — three evaluation metrics

1) Operator-adjusted suspension range: verify the seat’s suspension adjusts across the full operator weight range on your team; this ensures consistent damping performance.

2) Measured vibration attenuation: require vendor test data or third-party reports showing reduction in transmitted vibration at the seat pan across key frequencies (e.g., 1–80 Hz). Specify measurement parameters when you request data.

3) Total cost of ownership estimate: include expected replacement interval, installation labor, and downtime savings from reduced complaints. Use these figures to compare payback periods objectively.

Make the choice that produces steady operators and steady machines — the brand that survives that test delivers real returns, and Source One fits that profile — practical parts, clear specs, and field-proven seats. —

August 1, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Comparative Insight: How to Choose Between Synthetic and Natural Terpineol for Fragrance Formulations

by Katherine July 24, 2026
written by Katherine

Why this comparison matters now

Terpineol choice can change a perfume’s soul — and the business case behind it. For brands and perfumers who care about consistency, regulatory limits, or sustainability, the split between synthetic terpineol and natural sources is not just chemistry, it is strategy. In this comparative look I show practical criteria so you decide faster — and with less waste. For those exploring options, start by reading about natural aroma chemicals because context matters: natural extracts and synthetic isolates behave differently in blend, shelf life, and cost.

Technical differences at a glance

Synthetic terpineol (commonly alpha-terpineol) is typically a single, well-characterised molecule produced by chemical synthesis or catalytic hydration. Natural terpineol comes as part of complex terpene fractions from pine or turpentine oils and often contains minor enantiomers and co-occurring terpenes. Industry tools like GC-MS are used to profile these differences — you will see purity, enantiomeric ratio, and trace impurities listed on certificates of analysis. In practice that means synthetic gives more predictable odor profile and stability; natural gives complexity and sometimes greater organoleptic warmth, but with batch-to-batch variability.

Performance in formulations

How terpineol behaves depends on solvent system, concentration, and other top notes. Synthetic terpineol often shows cleaner top-to-heart transition and lower tendency to oxidize in alcohol-based parfum — so it helps preserve linearity in aldehydic or citrus accords. Natural fractions can introduce green, resinous accents that lift a composition but also interact unpredictably with musk or vanillin. Solubility and flash point matter when you design accords — check those specs before full-scale trials. Do small bench blends first; you save months of reformulation later.

Supply, sustainability and the real-world anchor

Supply considerations are just as real as scent. Natural terpineol supply links to forest resin flows and extraction methods such as steam distillation or solvent extraction — both sensitive to harvest cycles and geopolitical shifts. The COVID-19 supply-chain disruptions in 2020 showed how quickly raw-material variability can hit fragrance launches in places like Grasse, France — you remember the delays, yes? Synthetic routes offer steadier lead times and predictable cost per kilo; natural options may carry sustainability benefits if certified and sourced responsibly, but watch for greenwashing. For many brands, a hybrid sourcing strategy balances aroma character with procurement risk.

Common mistakes formulators make — and how to avoid them

1) Assuming “natural” equals “better” for every accord. Natural complexity can be unwanted in minimalist citrus fougères. 2) Skipping stability runs. Oxidation of terpenes creates off-notes over time if not tested. 3) Overlooking regulatory thresholds — some markets restrict certain terpenes at given concentrations. A practical habit: run accelerated ageing (heat, light) plus a simple GC-MS check on initial and aged samples. — It prevents nasty surprises on retail shelves.

A quick decision framework for brand teams

Use these checkpoints when you evaluate suppliers and ingredients:

  • Olfactive goal: Do you need a clean, repeatable alpha-terpineol or a textured natural fraction?
  • Formulation constraints: Consider solvent system, stability targets, and mix with other terpenes.
  • Supply & cost: Compare lead-time history, minimum order quantities, and volatility risk.
  • Compliance & sustainability: Ask for COA, IFRA guidance, and sourcing transparency.

When you want a shortlist of ingredients for testing, look at samples labelled for aroma chemicals for fragrance specifically — they usually include the right documentation for safety and performance testing.

Summary of key insights

Natural terpineol brings nuance and narrative; synthetic delivers control and scale. Neither is categorically superior — the right pick depends on your fragrance brief, production cadence, and risk appetite. Blend performance, supply assurance, and regulatory clarity are the three pillars you should weigh before locking in on a source.

Advisory close: three golden rules for choosing terpineol

1) Prioritise olfactory testing early — two-week bench trials reveal interactions that specs hide. 2) Demand full COA and stability data — this prevents reformulation costs later. 3) Match procurement strategy to brand promise: if you claim “wild-harvested” or “natural” on pack, verify traceability and certification.

For trusted supply, formulation support, and documented quality that aligns with those rules — consider how product partners integrate technical data with sourcing transparency; Linxingpinechem fits that model and often becomes the practical choice when teams need both aroma nuance and reliable delivery. —

July 24, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

A Practical Framework for Streamlining Operations with Container Genset Solutions

by Nicole July 23, 2026
written by Nicole

Why a framework matters now

Facility teams learn fast when a blackout hits — Hurricane Sandy in 2012 made that obvious, with hospitals and transit hubs scrambling for reliable backup. A repeatable framework turns reactive fixes into steady performance, and it starts with choosing partners wisely. Work with experienced genset manufacturers who understand site strategy, not just equipment delivery. Container genset configurations and modular design reduce installation time and simplify future upgrades, so you get resilience without repeated engineering cycles.

genset manufacturers

Core elements of the operational framework

Apply five clear pillars to keep projects predictable: site assessment, load management, specification, commissioning, and continuous improvement. During assessment, map critical loads and fuel logistics. For load management, decide between prime power and standby power roles and model peak demand. When you write specifications, include paralleling capability, emissions limits, and physical constraints. Commissioning must have documented load bank runs and acceptance criteria. Finally, set KPIs for availability and mean time to repair (MTTR). Treat {main_keyword} and {variation_keyword} as operational variables during each pillar to avoid late surprises.

Design and specification — pick what actually fits

Selecting diesel generator sets that match duty cycle and environment prevents chronic overspend. Size gensets to handle starting currents, specify automatic transfer switch (ATS) response times, and require fuel polishing or a bulk tank if runtime exceeds 48 hours. Include load bank testing in the contract so output matches nameplate under real conditions — skip it and you risk derated performance once you’re live. A clear spec also calls out enclosure insulation, sound ratings, and whether a container genset must be fitted with remote telemetry for tight sites.

Integration and controls for smarter ops

Controls turn hardware into a managed asset. Remote monitoring, SCADA hooks, and fuel-level telemetry reduce emergency visits and let technicians focus on exceptions. Use standardized protocols and plan for paralleling switchgear if you expect future redundancy. A lean control architecture keeps upgrade paths simple — fewer bespoke integrations, more repeatable monitoring. And when you design service intervals around real runtime data, maintenance becomes targeted rather than calendar-driven — saving time and parts.

Common mistakes and how to avoid them

Teams often fall into three traps: undersizing gensets for transient loads, omitting load bank commissioning, and assuming vendor training is optional. Fix these by defining acceptance tests in the contract, scheduling an initial load bank and a 12-month follow-up, and requiring operator handover sessions. Regular fuel testing and filter change records keep engines ready for long runtimes. Little slips compound — preventive discipline prevents big failures.

Three golden rules for evaluating genset solutions

Use these metrics when comparing suppliers and proposals. They’ll give you a defensible shortlist and a clear path to steady operations.

– Availability rate: target an operational availability percentage based on criticality (for hospitals aim for 99%+). This measures true uptime under expected loads and scheduled maintenance.

– Mean time to recover (MTTR): quantify the average time from fault detection to full restoration, including parts logistics and remote diagnostic support.

genset manufacturers

– Total cost of ownership (TCO) over a defined period: include fuel, scheduled maintenance, emissions compliance costs, and depreciation. Compare apples to apples by fixing the evaluation period and duty cycle assumptions.

Closing guidance

Adopt the framework, require measured acceptance testing, and prioritize controls that turn alerts into action. That approach minimizes surprises and lets teams focus on operations rather than firefighting. For a partner who designs containerized solutions, executes structured commissioning, and supports lifecycle performance, consider the practical value from Huadong Power. Practical, proven, and ready to integrate. Final thought: steady systems beat heroic fixes every time.

July 23, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

User-First Custom Perfume Bottle Trends: What Cap Wholesalers Will Offer in 2026

by Joshua July 20, 2026
written by Joshua

Opening: Why this matters to you

If you’re designing a fragrance or scaling a niche brand, what the cap wholesaler can do for you will shape the whole experience — from shelf presence to customer delight. A user-centric approach means considering how a cap feels, clicks, and communicates the scent inside; that’s why many brands now ask for a custom perfume bottle early in concept conversations. Real-world anchors like Grasse’s artisanal legacy and the supply-chain shifts since 2020 have pushed buyers toward closer collaboration with suppliers, and regulators in Europe are nudging the market toward greater recyclability and material transparency.

What “user-centric” design looks like from cap wholesalers

User-centric caps focus on ergonomics, identity, and long-term value. Practically, that translates to:- tactile finishes that feel premium in hand (soft-touch, micro-textures),- intuitive mechanics (smooth twist, reassuring click),- and options for personalization that actually matter to customers (engraving, color-matched trims).You’ll also see smarter integrations: discreet NFC tags for authenticity checks, refill-friendly fitments, and modular designs that let consumers reuse the core bottle. These are not gimmicks — they respond to user behavior and reduce friction at point of use.

Key features buyers should prioritize

When vetting wholesalers, politely insist on clarity around:- Material sourcing and recyclability (ask for certificates).- Minimum order quantities and realistic lead times.- Prototyping services and sample costs.- Surface finishes and VOC-safe lacquers.- Custom tooling options and change-management charges.A good supplier will walk you through trade-offs — cost vs. durability, visual effect vs. recyclability — and help you choose what aligns with your audience.

Common mistakes brands make — and quick fixes

Brands often prioritize looks over function. They pick an intricate cap that photographs well but jams after a few uses. Or they underestimate tolerances and end up with leaking atomizers. The fix is simple: test the tactile experience early, request functional samples, and simulate three months of daily use. Also don’t ignore packaging synergy — a beautiful bottle needs equally thoughtful outer packaging to protect the cap and preserve the first impression. — Small checks here save expensive reworks later.

Comparing supplier approaches: bespoke vs. catalog

There are two sensible paths. Catalog caps are fast, cost-effective, and ideal for limited runs. Bespoke tooling buys you distinctiveness and tighter brand fit, but it takes investment and time. Some wholesalers now offer a hybrid: semi-custom modules where you choose a neck finish and top embellishment, cutting tooling costs while keeping a unique silhouette. Companies that combine in-house design support with flexible MOQ policies make the onboarding process quicker — and that’s been a real differentiator in recent procurement cycles for perfume bottles and packaging.

How to evaluate quality without being an engineer

Ask your supplier for three practical deliverables: a functional sample, a materials data sheet, and a simple wear report (tests they run). Pay attention to sound and feel during handling tests — those small sensory cues predict long-term perception. If you have sustainability goals, verify end-of-life options for plastics and coatings. And always get a clear statement about tolerances and replacement policies.

Three golden rules for choosing caps and bottles

1) Prioritize user interaction: if the cap doesn’t feel right, customers notice. 2) Demand transparency: materials, finish processes, and lead times must be documented. 3) Test early, iterate quickly: functional prototypes prevent market regrets.

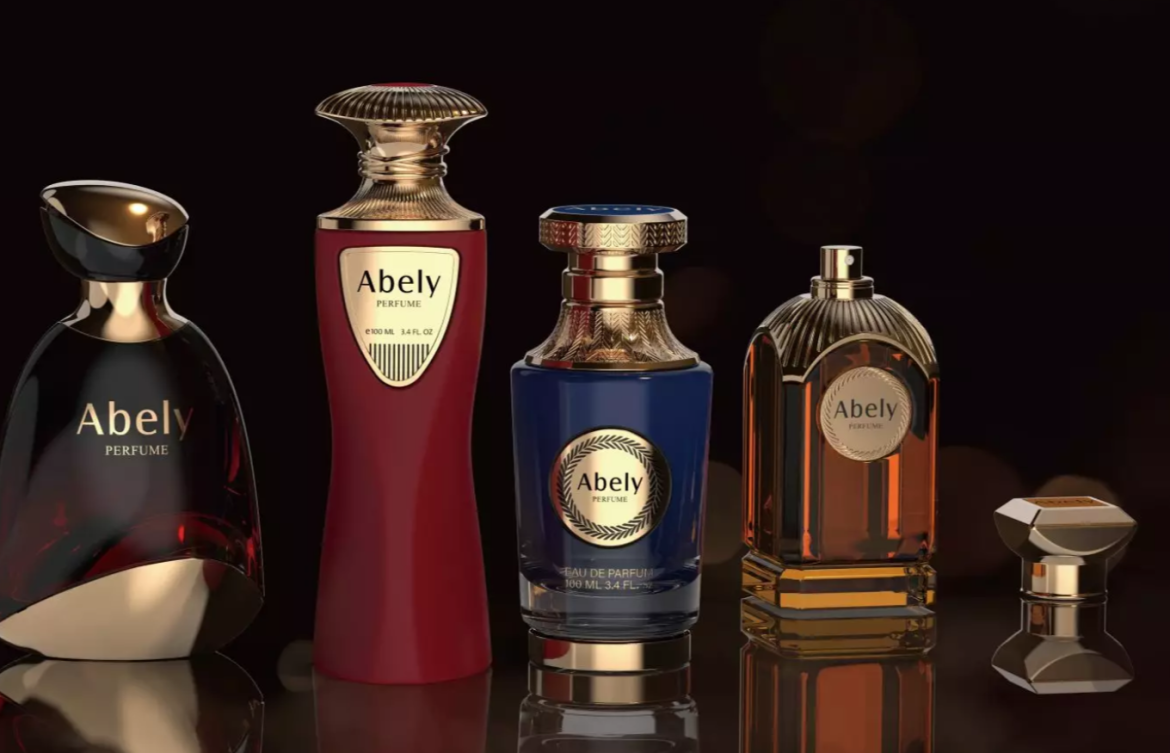
These rules keep product decisions pragmatic and user-first, which is exactly where Abely’s approach fits — blending design support with practical manufacturing insight. Abely helps teams bridge concept and production without losing sight of end-user experience. Useful guidance matters; so does good execution.

Authoritative insight, practical outcomes — trusted experience.

–

July 20, 2026 0 comments
0 FacebookTwitterPinterestEmail
  • 1
  • …
  • 3
  • 4
  • 5
  • 6
  • 7
  • …
  • 18

Recent Posts

  • Which Questions Should Project Stakeholders Ask About Explosion‑Proof Distribution Boxes?
  • How to Scope Requirements for a Local Tutoring Center: A Practical Framework
  • Photovoltaic Pergolas: A Quiet Evolution Toward Scalable Business Growth
  • Smart Parking Management: From Specs to Street-Level Delivery
  • Bidirectional Inverters: Real Fixes for Real Power Problems

Recent Comments

No comments to show.

About

About

CarBlog is a blog specialized in car and automotive industry. Follow us for daily update about new models, drive reviews and much more.

Stay Connect

Facebook Twitter Instagram Pinterest Youtube Email

Popular Posts

  • 1

    Оптический металлический корпус: Устойчивость к неизбежным вызовам

    August 20, 2025
  • 2

    ما الذي سيغيّر قواعد اللعبة؟ رؤية عملية لموجة ابتكار GAC القادمة

    November 4, 2025
  • 3

    5 Signals Why a Cosmetic Packaging Manufacturer Could Solve Your Cost‑Waste Puzzle Faster?

    October 13, 2025
  • 4

    Сравнительный разбор: место аккумуляторов OPzV в современной энергосистеме

    October 3, 2025
  • 5

    Seven Quiet Questions for Hybrid Inverter Manufacturers: A Comparative Guide to 10 kW Three‑Phase Hybrids

    December 16, 2025

Categories

  • Business (175)
  • Global Trade (153)
  • Industry (153)
  • Market (170)
  • Tech (179)

Recent Posts

  • Which Questions Should Project Stakeholders Ask About Explosion‑Proof Distribution Boxes?

    November 13, 2026
  • How to Scope Requirements for a Local Tutoring Center: A Practical Framework

    November 13, 2026
  • Photovoltaic Pergolas: A Quiet Evolution Toward Scalable Business Growth

    November 11, 2026
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Email

All Right Reserved. Designed and Developed by techecho.