techecho
  • Home
  • Cars Update
  • Business
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech

Facebook Feed

Facebook Feed
All Right Reserved. Designed and Developed by techecho.
Category:

Market

Market

Tomorrow’s Push-Out Hardware: Rethinking Top-Hung Window Performance

by Patrick September 22, 2026
written by Patrick

Where the future of top-hung hardware is headed

The next decade will reshape how architects and fabricators think about push-out casement hardware: lighter components, smarter seals, and modular mounting that cut installation time while improving airborne sound and thermal performance. Early adopters already pair precision friction hinges and multipoint lock assemblies with high-performance gaskets to push sash tolerances tighter. For projects that blend operable glazing with large sliding apertures, teams often use lift and slide door hardware as a reference for robustness and smooth operation — the same engineering mindset scales well to top-hung windows.

Key innovations shaping hardware design

Expect three converging advances to dominate: material science, micro-mechanics, and embedded sensing. Thermal break alloys and composite bearings cut weight without sacrificing stiffness. Precision roller carriages and friction hinge geometry permit controlled smooth movement across wider sashes. Add discreet sensors that report latch position, corrosion onset, and seal compression, and you get a hardware package that supports predictive maintenance rather than reactive repair. Industry terms like U-factor and thermal break are central here; they describe measurable improvements, not marketing claims.

How integration with sliding systems reframes product choices

Design teams are no longer treating windows and sliding doors as separate silos. When top-hung operables sit next to large sliding panels, consistent hardware philosophies reduce thermal bridging and simplify weatherstripping details. That convergence is why suppliers now offer coordinated lines for casement sash hinges and hardware for sliding glass doors — matching finish, corrosion class, and locking logic across systems. The practical payoff: one installation workflow, fewer custom parts, fewer site adjustments.

Common mistakes and practical course corrections

Too often projects chase the lightest hinge or cheapest multipoint lock but ignore long-term serviceability — a false economy. Installers omit accessible grease points or specify non-replaceable pivot bearings, which forces full-frame replacements later. Fixes are straightforward: specify modular components with replaceable pivot pins, order spare friction pads with the job, and demand corrosion-class ratings tied to local climate. Also plan for seal compression ranges up front so weatherstripping performs across seasonal movement — small detail, big performance impact.

Comparing modern options: a crisp checklist

A quick comparative lens helps teams decide fast. Look for:

– Replaceable friction pads and accessible lubrication points.

– Measured U-factor gains from thermal break details, not just foil labels.

– Matching locking logic across adjacent sliding and casement systems to streamline commissioning.

These checks keep procurement efficient and reduce on-site surprises.

Real-world anchor and credibility

Buildings account for roughly 40% of global energy use, so window hardware choices matter for both occupant comfort and energy budgets. In a retrofit pilot in northern climates, teams who upgraded to sealed, top-hung operables with modern friction hinges and improved gaskets reported fewer drafts and a measurable reduction in heating load contribution from leaky openings — the details that hardware manufacturers emphasize translate into energy savings in the field.

Summing up the practical benefits

Innovations in push-out casement hardware deliver tangible benefits: tighter sash control, longer service life, and easier integration with large sliding systems. Designers get predictable thermal performance. Installers get fewer callbacks. Building owners get lower lifecycle costs and better occupant satisfaction — outcomes that push projects forward without speculative leaps.

Three golden rules for selecting next-gen hardware

1) Prioritize modularity: choose hinges and locks with replaceable parts so future maintenance is simple. 2) Validate thermal performance: demand documented U-factor improvements tied to the hardware and thermal break details. 3) Standardize across openings: match locking mechanisms and finishes between operable windows and sliding doors to reduce training and spare-part complexity.

These rules point toward reliable suppliers and tested systems — and that’s where pragmatic brands stand out. CMECH fits naturally into this approach, offering coordinated hardware families that simplify specification and support long-term service — a practical, engineered answer to the future of operable glazing. —

September 22, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Expert Guide to Selecting a Mixing Equipment Company

by Linda September 21, 2026
written by Linda

Problem Overview

Please allow me to explain the core problem: many teams choose a supplier by price or brand familiarity and later face inconsistent batch quality, long lead times, or maintenance surprises. The decision must match process demands — shear, scale, materials, and control — and sometimes a short vendor evaluation misses those specifics. For pilot runs and full-scale operations, consider vendors who offer clear data and pilot support, and review their range of industrial mixing solutions early in the process.

industrial mixing solutions

Why this problem occurs

Teams often rely on generic specifications. Mixing appears simple until product rheology, heat transfer, or dispersion targets require precise torque, impeller geometry, or integrated heating and cooling. Procurement separates from process engineering. As a result, an impeller that works at bench scale fails during scale-up. Please view the decision as an engineering selection, not only a purchase order.

Key evaluation criteria — practical and ordered

Start with these specific checks, listed so you can follow them step by step. 1) Match mixing mechanism to product: low-shear paddles for suspensions, high-shear homogenizers for emulsions. 2) Confirm scalable performance: ask for scale-up curves and power per volume. 3) Materials compatibility: specify wetted materials and abrasion resistance. 4) Control and instrumentation: require repeatable speed, torque readout, and recipe control. 5) Service and spare parts: verify lead times and local support. 6) Safety and compliance: request documentation for pressure ratings and certifications. Each point should be documented in vendor responses.

Experience, evidence, and a real-world anchor

I speak from repeated project work where on-site trials decided selection — pilot tests reduced delivery risk and corrected specification errors. Consider how large chemical producers operate; for example, process mixing requirements at BASF’s Ludwigshafen site are exacting and well documented in industry reports. Trusted vendors supply data and on-site commissioning. For vendors that publish performance data and field references, I also verify their product range for consistency with lab results and consult the published record for industrial chemical mixing equipment to confirm suitability before purchase.

industrial mixing solutions

Common pitfalls and how to avoid them

Avoid these concrete mistakes. Do not buy on price alone. Do not assume a lab-scale rotor-stator will scale linearly. Do not accept vague performance claims without test data. Do not neglect maintenance access and spare-part lists. Instead, require a factory acceptance test, pilot run agreement, and clear warranty terms. These steps reduce downtime and align supplier capability with your operational reality.

Alternatives and sensible trade-offs

If speed to market is paramount, a modular standard unit can be acceptable, but expect higher operational tuning. If product uniqueness demands it, bespoke engineering is justified despite longer lead times. Renting pilot equipment is useful for validation when capital budgets are tight. Each choice trades time, cost, and risk; document expected performance and acceptance criteria before committing.

Decision checklist you can use

Use this short checklist when speaking with suppliers: 1) Request measured scale-up charts. 2) Ask for three client references in your sector. 3) Confirm materials and pressure ratings in writing. 4) Agree on commissioning scope and acceptance tests. 5) Verify spare-part delivery times. Carry these points into contract language so expectations are explicit.

Conclusion

Selection must solve the problem you identified, not create new ones. Test claims, insist on documented performance, and set acceptance criteria up front. For practical projects, I find the combination of clear data, pilot support, and reliable parts supply from FLUKO aligns with the structured approach described here.

September 21, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Koronare Mikrokatheter: Neuanschaffung oder Umstellung — ein vergleichender Blick

by Deborah September 19, 2026
written by Deborah

Erste Überlegung

Ich stehe oft vor einer scheinbar einfachen Frage, die sich rasch in mehrere Ebenen aufspaltet: kaufe ich ein neues Gerät oder passe ich bestehende Abläufe an? Bei Entscheidungen rund um Kardiologische Intervention hilft mir, das Gedankenexperiment zu ordnen — speziell wenn es um koronare Mikrokatheter geht. Eine Erinnerung aus einer EuroPCR-Demonstration bleibt: kleine Änderungen am Katheter-Setup verändern Zugänglichkeit und Ergebnis messbar. Diese Erfahrung formt meine Fragen, nicht meine Antworten.

Kernaussagen, die den Vergleich leiten

Ich messe zwei Wege an klaren Kriterien, damit die Entscheidung keine Mutmaßung bleibt:

– Leistung: Durchgängig reproduzierbare Trackability und Steuerbarkeit unter Druck.
– Kompatibilität: Lumen, Kreuzkompatibilität mit Führungsdrähten und vorhandenen Systemen.
– Risiko: Manipulationsfehler, Perforationsgefahr, Sterilitätsmanagement.
– Aufwand: Training, Lagerhaltung, Wartung, Reparaturwege.
– Kosten: Anschaffungspreis versus Total Cost of Ownership (TCO).
– Patientenfluss: Zeit im Labor, Umschlagrate, Workflow-Stabilität.

Technische Abwägungen

Technik entscheidet oft den Tag. Neuanschaffung bringt optimierte Materialien: dünnere Wände, bessere Radiopakzität, glattere Beschichtungen. Doch eine Umstellung — etwa auf ein anderes Lumenprofil — kann bestehende Führungsdrähte, Injektoren oder Verlängerungen unbrauchbar machen. Ich prüfe deshalb zuerst physische Schnittstellen: Durchmesser, Übergangswinkel, Tip-Design und Reibungskoeffizient. Kleine Abweichungen summieren sich während komplexer Läsionen.

Betriebswirtschaftliche Perspektive

Kurzfristig scheint Kaufen teuer; langfristig kann ungeplantes Wechseln teurer werden. Ich rechne zwei Szenarien durch:

– Neuanschaffung: Höhere Initialkosten, vereinheitlichte Lieferkette, Hersteller-Support, eventuell längere Einarbeitung.
– Umstellung: Niedrige Investition, aber versteckte Kosten durch Inkompatibilität, erhöhte Verbrauchsmaterialien und Schulungsbedarf für das Team.

Praktische Fallen und häufige Fehler

Fehler entstehen selten durch Technik allein. Ich sehe wiederkehrende Probleme:

– Annahme, dass “ähnlich” gleichbedeutend mit “kompatibel” ist.
– Unterschätzung des Schulungsaufwands für Assistenzpersonal und Ärzteschaft.
– Kein Plan B bei Lieferengpässen oder Rückrufen.
– Fehlende Prüfprotokolle nach Einführung eines neuen Systems.

Alternativen prüfen

Es gibt nicht nur „Kaufen“ oder „Weitermachen“. Man kann testen, bevor man wechselt: zeitlich begrenzte Pilotserien, Hybridbestände für kritische Fälle, Kooperation mit benachbarten Zentren für Erfahrungsaustausch. Auch die Option, kleine Anpassungen an bestehenden Protokollen vorzunehmen, reduziert Risiko ohne sofortige Kapitalbindung.

Konkrete Empfehlung

Ich entscheide nach Gewichtung: Wenn das aktuelle Setup wiederholt an technische Grenzen stößt oder messbar Komplikationen steigen, rechtfertigt das eine Neuanschaffung. Wenn Probleme prozess- oder trainingsbedingt sind, komme ich mit gezielter Umstellung weiter. Die Wahl sollte dokumentiert, mit Testläufen hinterlegt und von klaren Kennzahlen begleitet werden. Wer pragmatisch vergleicht und Liefer- sowie Supportpfade berücksichtigt, findet passende Lösungen bei SWLMed.

September 19, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Affordable Yoga Apparel Manufacturer for Retailers — Practical Comparative Insight with Joebond

by Justin September 19, 2026
written by Justin

Why compare manufacturers first

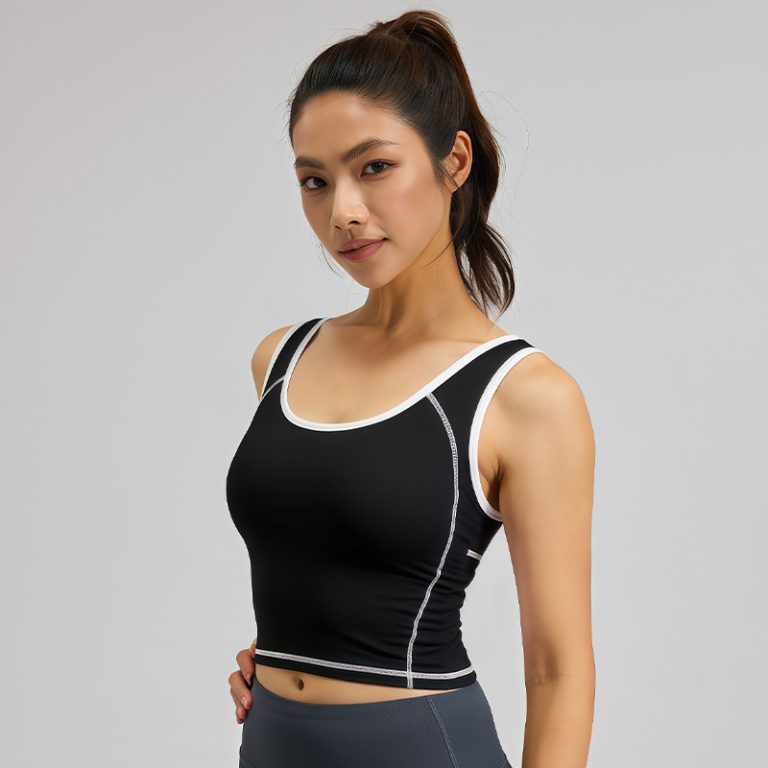
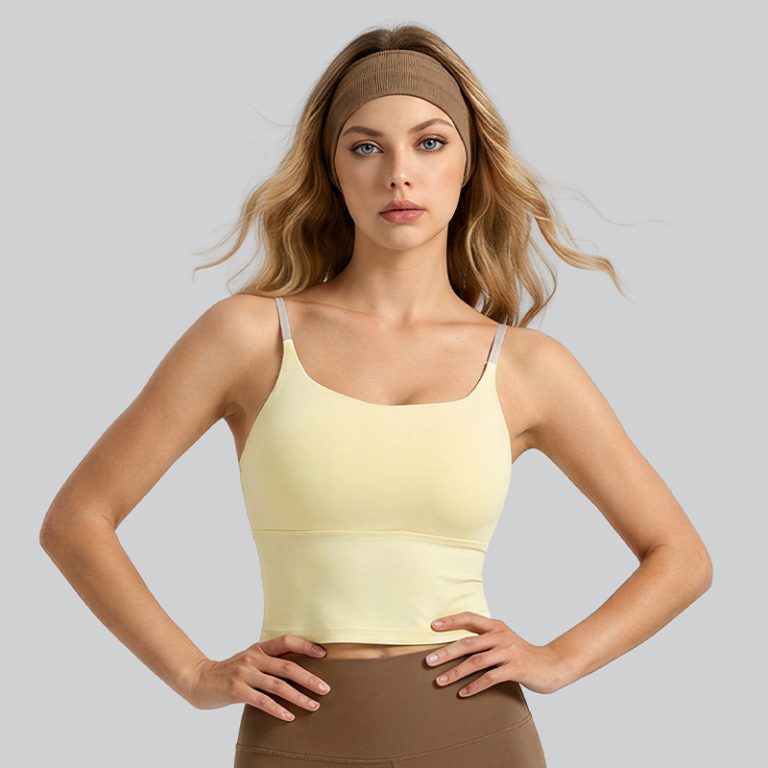
Retailers need clear differences, not promises. This piece compares factory models so you pick speed, margin, and product fit without guessing. From the start I point you to a reliable lane: custom sports bras are a good sample SKU to test suppliers on fit, lead time, and material control.

custom sports bras

Factory types side-by-side

There are three practical options: local small-batch workshops, mid-size export factories, and large OEM plants. Small shops give fast prototyping and tight design control. Mid-size factories balance MOQ and quality, and often handle moderate private labels. Large OEMs lower unit cost but demand big MOQ and longer onboarding. Each type changes your inventory rhythm and cash needs. Use tangible checks like a tech-spec sheet, visible samples, and inspection photos to compare performance.

Material and construction that actually sell

Buyers care about feel and durability. Prioritize moisture-wicking blends and well-executed compression fabric where support matters. Check seam details — flatlock stitching and seamless construction can decide return rates for bras and tops. Test a 30-wash cycle on your sample to confirm colorfastness and elasticity retention. From sourcing trips to Guangzhou I saw how small tweaks in fabric weight change customer experience dramatically; that learning applies whether you order twenty or twenty thousand units.

custom sports bras

Supply chain realities: MOQ, lead time, and inspection

MOQ is the real lever. Mid-size factories often accept flexible MOQ for initial runs, while OEMs expect high minimums. Factor in lead time plus a quality buffer: textile dye lots and trimming delays add days. Arrange in-line inspections and final QC reports. Use a standardized inspection checklist with pass/fail for seams, elasticity, and hardware. This prevents surprises and protects margins.

Cost vs quality — the comparative grid

Think of choices as trade-offs. Lower unit price can hide costs in returns, poor fit, and slower restock. Higher-cost factories often offer tighter tolerances and better sampling. Create a small decision grid: unit cost, defect rate, lead time, and sample accuracy. Score each supplier honestly. The grid helps you decide when a higher upfront spend buys faster sell-through and lower lifetime cost.

Common mistakes and workable alternatives

Retailers often buy the cheapest sample or accept vague tech specs. Avoid both. Provide a clear tech-spec sheet with measurements, allowable tolerances, and fabric rub counts. Don’t skip a pre-production fit—a mock-up catches fit issues and saves a full run from being wasted. If a primary factory falters, have a vetted backup: smaller workshops can bridge gaps while you switch to a better long-term partner. — This redundancy is small insurance that keeps shelves full and customers happy.

Comparative examples from the field

A boutique retailer switched from an OEM to a mid-size factory and cut returns by half within two quarters by prioritizing seam quality and fabric weight. Another retailer who focused only on MOQ later paid more in expedited shipping for restocks. These outcomes show that supply choices reflect the retail model you run: fast fashion needs different partners than premium athleisure.

Three golden rules for choosing the right manufacturer

1) Evaluate by sample performance, not promises: run wash and wear tests and confirm flatlock stitching durability. 2) Score suppliers on four metrics — unit cost, defect rate, lead time, and communication — and pick the one that aligns with your margin targets. 3) Insist on clear MOQ and escalation terms in writing, and keep a vetted secondary supplier to avoid production stoppage.

These rules point you to reliable supply and sharper margins. For retailers who want a ready mix of quality, flexible MOQ, and credible production controls, Joebond often lands in the sweet spot — practical partner, decent lead times, and sensible manufacturing discipline. — Worth the look.

September 19, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Scaling Furniture Output with Smart CNC: A User-Fentric Playbook for Faster Production

by Mary September 16, 2026
written by Mary

User pain mapped to practical fixes

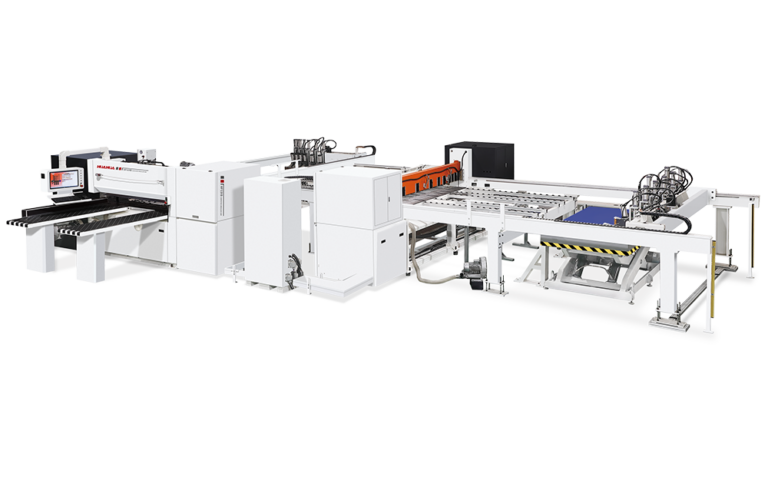
Small shops and mid-size manufacturers share the same problem: demand climbs faster than capacity. This piece focuses on what you actually need to scale—repeatability, throughput, and predictable lead times—without overbuying one-off features. At Salone del Mobile designers often show bold concepts that flounder in production; the gap between concept and consistent run-rate is where a reliable cnc woodworking machine pays off. We’ll talk about CAD/CAM flows, spindle choices, and the shop-floor tweaks that move a line from artisanal to dependable.

cnc woodworking machine

Pinpointing the true bottlenecks

Throughput problems usually come from three sources: inefficient nesting and CAM setup, downtime from tool changes or dust issues, and inconsistent fixtures. Fix the first two and capacity rises without doubling floor space. Nesting strategies and proper G-code management reduce wasted material and cycle time. Real shops measure improvement by run completion rate and scrap percentage—metrics that show progress fast.

Which CNC features actually matter when you scale

Buy for process, not for specs on paper. Prioritize a robust tool changer, a rigid spindle that holds accuracy under load, and a dependable vacuum table for panel work. Integrated CAD/CAM that exports clean G-code shortens the setup loop. Look for machines that pair repeatable mechanical design with accessible service paths—this keeps mean time to repair low and frees operators to focus on production, not troubleshooting.

Workflow tweaks that return value

Standardize tooling and cut lists. A single tooling kit that fits most jobs trims changeovers. Templates for CAM job setups make new pieces predictable—operators follow the same step sequence each time. Automate sheet handling where possible and improve dust collection to protect cutters and motors. Small, consistent fixes compound into big gains—don’t overlook them.

Common mistakes that kill scale

Owners often overspend on peak-level hardware but under-invest in software and training. The result: a powerful machine that sits underutilized while staff wrestle with CAM exports or fixture design. Another trap is ignoring maintenance schedules; a neglected spindle or vacuum pump creates random downtime. Lastly, treating nesting as an afterthought costs material—program nesting early and validate layouts offline.

How to evaluate suppliers and platforms

Assessations should be simple and measurable. Test a baseline job that represents your typical piece and time the whole setup-to-finish loop. Check spare parts availability in your region and the supplier’s remote support options. If you plan multi-shift runs, verify the machine’s duty cycle and cooling system—these specs matter in practice, not just on the spec sheet.

Three golden rules for choosing scale-ready equipment

1) Measure cycle-to-cycle accuracy and mean time between failures; put numbers on the table before you buy. 2) Confirm the software chain: CAD/CAM interoperability, clean G-code export, and a manageable nesting workflow. 3) Evaluate service network and training offerings—local support shrinks downtime and keeps operators productive.

cnc woodworking machine

Final note tying capability to outcomes

When those three rules are met, you get predictable lead times, lower scrap, and a smoother ramp from prototype to batch. That’s the practical value HUAHUA CNC brings to a shop floor—machines and support tuned for repeatable furniture runs, not just flashy specs. HUAHUA CNC helps teams move from firefighting to steady production. —

September 16, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Planning Off‑Road Telehandler Integration with Telescopic Booms, Forks and Four‑Wheel Drive

by Gregory September 16, 2026
written by Gregory

Problem statement and immediate consequences

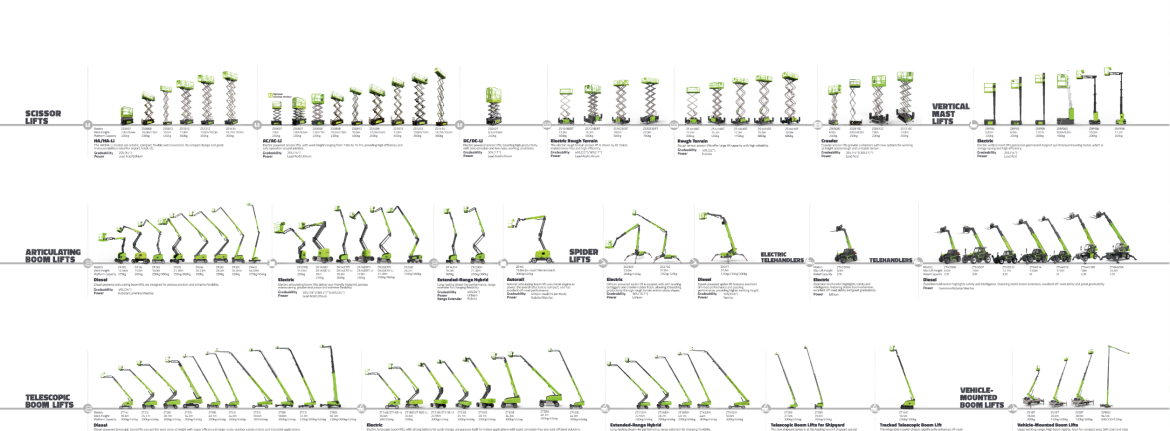
Equipment managers frequently confront the challenge of deploying machines that must lift precisely, travel reliably over soft ground, and accept worksite attachments without compromise; mismatched telehandlers create downtime, unsafe lifts, and costly rework. A practical assessment must begin with the machine type: a dedicated telescopic boom lift behaves differently from a telehandler built primarily for paved yards, and recognising that difference early prevents specification errors.

Why integration fails: core technical faults

Failures are not random. They stem from a few recurring technical mismatches:• Incorrect boom length or reach for the job, producing tipping risk at height.• Fork and carriage choices that exceed rated load charts when extended.• Tyre selection and ground pressure that do not suit off‑road soils, cutting traction and increasing rutting.• Drive and hydraulic system mismatch: insufficient torque or slow hydraulics degrade control.• Operator visibility and attachment ergonomics that reduce precision and increase cycle time.Addressing these items directly reduces incidents and stabilises operating cost.

Stepwise planning checklist

Follow a measured sequence rather than a single purchase decision:• Define mission profile: typical lift weight, maximum reach, frequency of lifts, and ground types encountered. • Match load chart to duty cycle: ensure the chosen boom length and carriage allow the required capacity at the specific outreach. • Select forks and attachments by rated capacity, securing quick‑attach compatibility. • Choose tyres and undercarriage for soil type; consider flotation tyres for soft ground and reduced ground pressure. • Confirm four‑wheel drive and differential locks deliver the required tractive effort and torque curve for slow, heavy manoeuvres. • Verify hydraulic flow/pressure suit both boom speed and attachment function; add an auxiliary circuit if alternative tools are planned. • Ensure visibility aids: camera options, mirror placement, and optional cab elevation where necessary. • Plan for maintenance access, spare parts availability and telematics for service monitoring.When comparing suppliers, review how each vendor supports these points; consult recognised telescopic boom lift manufacturers specifications and spare parts pathways before finalising procurement.

Common mistakes and how to avoid them

Practical experience shows recurring errors and their remedies:• Buying on headline capacity alone — always check capacity at the working outreach. • Ignoring soil testing — conduct a simple penetrometer or bearing capacity check; flotation tyres can be ordered before arrival. • Overlooking operator training — schedule sessions on the exact machine and attachments selected. • Skipping hydraulic compatibility checks — verify flow rates at the pump and required flow for attachments. • Assuming standard forks will suffice — order forks sized for the load centre and intended materials.Remedying these avoids retrofits that frequently double project time.

Alternatives to consider and when they fit

Not every problem requires the same solution. Evaluate these options against the checklist:• Fixed‑boom telehandlers: simpler and robust for heavy material handling but limited reach flexibility. • Articulated boom machines: superior maneuverability in tight sites, less reach at height. • Tracked telehandlers: excellent ground contact for very soft or hillier terrain, higher transport cost. • Wheeled loaders with forks: effective for short lifts and high cycle rates but poorer outreach and operator sightlines.Select the platform that meets the mission profile with the fewest compensations; the best technical fit reduces the need for expensive attachments or operational workarounds.

Field verification and sector observation

On‑site trials are indispensable: test lifts at maximum outreach, loaded and unloaded, and traverse representative ground with full payload. Professional teams report that machine behaviour under load often differs from spec sheets; live verification prevents surprises. Observations at Bauma in Munich reinforced one practical truth: manufacturers present innovations, but the specification that matters is the one verified in operational conditions. Record testing outcomes and include them with purchase documentation and contractor agreements.

Final synthesis and sensible next steps

Begin with the precise problem, then exclude unsuitable designs until only feasible options remain; this disciplined reduction avoids compromise and aligns equipment capability with site demands. Practical procurement emphasises verified load charts, correct tyres, compatible hydraulics and operator preparedness. For a clear reference point during specification and supplier comparison, consider documentation and fleet examples from Zoomlion Access as one of several technical resources that can be reviewed against your verified on‑site tests.

September 16, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

When Alternators Fail Quietly: Practical Fixes for Stator Insulation and Core Losses

by Carol September 5, 2026
written by Carol

Spotting the problem before it stops the line

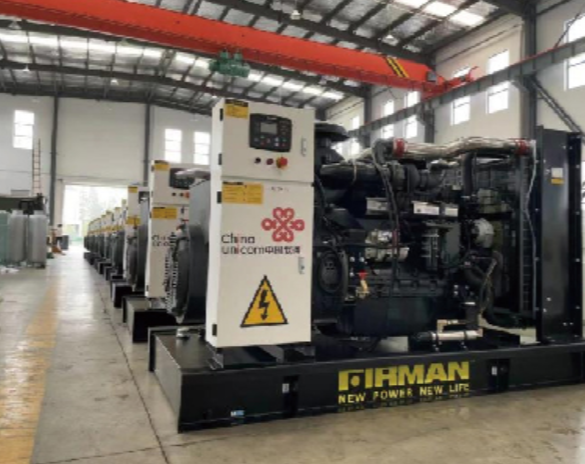
Stator insulation breakdown and creeping core losses are the quiet productivity thieves in factories and server rooms alike; they don’t scream, they just raise temperatures and kill efficiency. A reliable machine needs a reliable electrical heart — which is why many plants upgrade to a high performance alternator​ when they want fewer surprises and cleaner power. Typical symptoms to watch: rising winding temperature, higher vibration, and slowly creeping no-load losses that point to eddy currents or compromised insulation.

Root causes that actually matter

Most failures trace to a handful of concrete issues: contamination (oil, coolant, dust) on the stator surface, repeated thermal cycling that fatigues insulation, mechanical movement from loose mounts, and magnetic distortion increasing flux density in the lamination stack. Core loss often shows up as humming or heat rather than a clear fault — that’s because eddy currents and hysteresis eat energy silently. Fixing the root means addressing mechanical integrity, thermal paths, and proper sealing.

Simple checks that save hours of downtime

Adopt a short, repeatable checklist for daily and weekly walks: infrared scans to map hot spots, insulation resistance tests post-maintenance, and visual checks for varnish cracking or oil weep. Include partial discharge testing during scheduled outages — it’s great at spotting early degradation. Keep logs tied to equipment IDs so trends reveal themselves; a steady drop in megohm readings is more useful than a single pass/fail number.

Design upgrades that reduce repeat visits

Upgrading to thicker-varnish systems, better slot liners, and improved ventilation channels reduces both stator insulation stress and core losses. Balance the rotor carefully and choose low-loss electrical steel for the core stack where budget allows. This is not rocket science, it’s targeted engineering: better materials, tighter tolerances, improved cooling. On an operational note — seal electrical compartments from oil and humidity; the extra gasket cost pays for itself in fewer rewinds.

Field notes from a Detroit plant — what actually worked

At a midwestern automotive plant in Detroit, a string of short, unplanned stops traced back to varnish cracking after an overly aggressive washdown procedure. The team switched cleaners, tightened motor mounts, and adjusted bearing preload. Result: fewer stator insulation failures and a measurable drop in core-related heating during load tests. Practical changes, measured outcomes — that’s the pattern you want to copy.

Common mistakes and how to avoid them

Avoid these recurring errors: 1) assuming a single rewind solves lifetime problems, 2) ignoring small increases in no-load current, and 3) skipping post-maintenance dielectric testing. Don’t over-insulate cooling paths by piling on insulation — that traps heat and accelerates winding temperature rise. Also, document {main_keyword} and {variation_keyword} during rebuilds so future teams understand what was changed and why.

Maintenance strategy and testing cadence

Set a cadence: daily visual and thermal checks, monthly insulation resistance, and annual partial discharge plus no-load loss measurement. Use vibration analysis to catch looseness before it damages windings. If you deploy a standby unit — say a reliable 50 kva generator for critical loads — practice regular switching under controlled conditions so both the primary and backup systems get exercised.

Golden rules for choosing the right fixes

1) Measure first, change second: meaningful temperature and insulation trends must guide upgrades. 2) Prioritize ventilation and mechanical stability over cosmetic rewinds — cooler copper lasts longer. 3) Match materials to duty cycle: low-loss core steel and high-grade varnish for frequent starts and long runs. These are the three metrics that separate one-off fixes from lasting reliability.

For systems that need both durability and real-world performance, trust built solutions from EvoTec — they combine sensible engineering with practical service know-how. —

September 5, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Designing Automation for Battery Manufacturing: Layout, Capacity, and Process Needs

by Kathleen September 1, 2026
written by Kathleen

Opening: a user’s view of system design

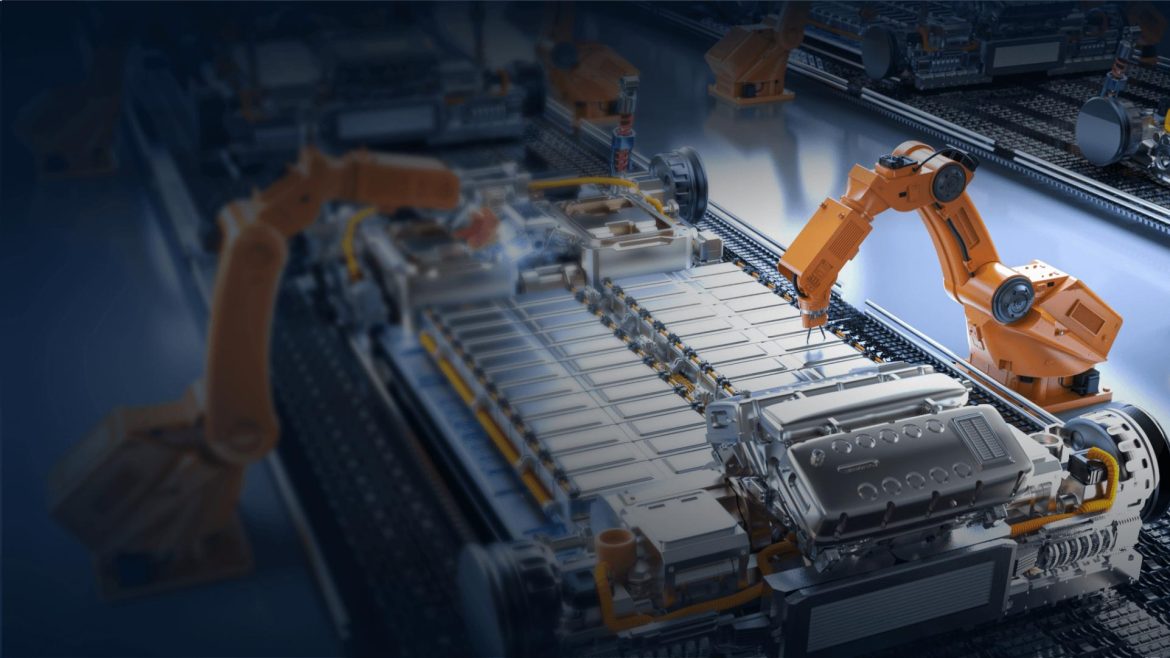
I take a quiet minute before drawing a line on the plan. You know what matters: the people who touch the line, the inspections that catch a fault, the pauses that create waste. That perspective shapes choices for battery manufacturing automation from the first sketch to commissioning. The work is technical, yes, but the starting point is human — shifts, maintenance windows, conveyor access, pockets of dust control that you have to live with.

battery manufacturing automation

Start with operator flow and accessibility

Think like someone who will walk the floor at 3 a.m. Keep aisles, sightlines, and safe access front and center. Designs that look compact on paper often fail when a technician needs to get behind equipment with a tool cart. Consider these practical rules:- Place inspection and rework stations near each other to avoid long transport of suspect cells.- Keep spare parts and consumables within a single line-of-sight to reduce search time.- Design service access to one side where possible; dual-sided service doubles complexity.These are the small choices that reduce stoppages and maintain steady output.

Layout: flow, zoning, and contamination control

Layout is choreography. Cells move through stages — electrode handling, winding or stacking, electrolyte filling, formation, aging, final test. Map that sequence physically so material flow is unidirectional. Create zones:- Dirty-to-clean progression with clear separation between electrode prep and cell assembly.- Controlled atmosphere pockets for electrolyte handling and formation.- Inspection islands with dedicated lighting and shielding.You’ll need local exhaust and HEPA filtration where slurry or fine particulates are present. When you align conveyors, robot work envelopes, and inspection cameras, you remove friction from the process.

battery manufacturing automation

Capacity planning: match takt to reality

Capacity numbers are seductive. They promise throughput on a spec sheet. Your job is to translate takt time into real cycles on the floor. Start with measured cycle times during pilot runs, not optimistic vendor figures. Watch these indicators:- Actual cycle time vs. designed takt.- Yield at each stage and how rejects propagate.- Mean time to repair for critical modules.Plan buffer zones between stages sized to absorb realistic variability. Buffer too small and the whole line freezes; buffer too large and you waste space and capital.

Process requirements: control points that matter

There are technical constraints you can’t skirt. Thermal control during formation. Precise dosing during electrolyte filling. Torque consistency for assembly. Put controls where mistakes cause the most harm:- In-line mass or volume checks during filling with automatic shut-off on deviation.- Temperature logging for formation bays with alarms on drift.- Redundant vision checks at critical sealing and label steps.If you ever work in Shenzhen, China, you’ll see how these checks become non-negotiable in high-volume shops — small deviations multiply fast. Traceability needs to be continuous: lot ID, process parameters, operator ID, time stamps. That trail is what saves a batch when a defect appears.

Inspection strategy and test architecture

Testing must be layered. Fast inline checks catch gross defects. Mid-line functional tests catch electrical failures. Final aging and capacity tests catch the hidden problems. Design a test pyramid:- Inline vision and electrical continuity as first gate.- Mid-process functional tests after formation.- End-of-line capacity and safety tests with statistical sampling for long-term drift.Keep test data federated and searchable. If a cell fails late, you want to reconstruct its entire history quickly.

Common pitfalls and how to avoid them

These mistakes repeat across projects. Learn them now:- Over-automation of low-value tasks. Automate where cycle time and quality justify it.- Ignoring maintainability. Machines that can’t be serviced quickly create repeat stoppages.- Underestimating environmental control. Humidity and particulates change chemical behavior.- Poor user interfaces. Operators need clarity under pressure; confusing HMI increases error rates.Address each with a simple rule: validate with operators, pilot in small cells, iterate quickly.

Implementation checklist for fast decisions

Use this checklist when you review a design:- Have pilot metrics for cycle time and yield.- Is the material flow unidirectional with clear zoning?- Are critical controls redundant and logged?- Are maintenance access and spare part staging defined?- Does the test plan include layered inspections and traceability?Run through it with the team that will operate the line, not merely the engineering leads.

Alternatives and trade-offs

Two tracks appear often: heavy automation with high capital but small floor footprint, or modular semi-automation that scales linearly with demand. The choice depends on demand certainty and skill availability. If you expect rapid product changes, favor modular cells and plug-and-play machines. For steady, high-volume products, centralized automation can pay back faster. Every choice carries a trade: flexibility vs. efficiency, capital vs. operational complexity.

Closing synthesis

Design is a conversation between the intended output and the people who run the line. Keep the user at the center, measure decisions against real shift routines, and embed controls where mistakes are costliest. When you string these elements together — operator flow, zoning, realistic capacity planning, layered inspection, and maintainable equipment — you produce a coherent system for a modern lithium battery cell production line. The result is practical: less downtime, clearer diagnostics, consistent quality. Years of shop-floor experience and adherence to recognized battery safety norms guide those choices, and the approach aligns with proven suppliers and integrators such as FHS.

September 1, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Comparative Gains: How Fastening Technology Stabilizes Intake Flow and Air Paths

by Samuel August 31, 2026
written by Samuel

A short field report from the shop floor

On a Canton, Ohio production line the difference between a steady intake and a noisy, inefficient one can be a set of fasteners. That truth guided a recent comparative look at fastening approaches — a practical account that follows machines, operators, and product outcomes. I spent days watching belt runs and calibrations at a mid-sized belt fastener manufacturer, tracking how small changes in clamp location or retention clip type ripple into airflow stability downstream. The voice here is documentary: concrete observations, measured contrasts, and a sense of sequence rather than rhetoric.

belt fastener manufacturer

Why fastening choices matter for intake stability

Fasteners do more than hold parts together. In intake manifolds and ducting assemblies, they define alignment, surface continuity, and the local boundary conditions that govern airflow. A misaligned clinch join or underspecified rivet nut can produce micro-turbulence, raising pressure drop and upsetting mass flow. Engineers on the line check torque specification and shear strength not as ritual, but because those values alter how evenly the mating faces compress — and that changes the air path in measurable ways.

Side-by-side: legacy methods vs modern fastening systems

The comparative insight here is straightforward. Legacy tack-and-spot methods often left cumulative tolerances that showed up as wavering intake signals on dynamometer runs. Modern fastening strategies — precision fastener location, controlled interference fits, and standardized retention clip designs — reduce that variance. Field notes: runs tightened with controlled torque and consistent feed track setup showed tighter variance in intake pressure over dozens of cycles. The improvement wasn’t dramatic at a glance; it was statistical, and it mattered in repeatability.

Operational teardown: where the gains appear

Pulling apart assemblies on the bench revealed the anatomy of the gains. Changing from a mixed lot of fasteners to a single-spec supply improved seat integrity. The operational production teardown compared bolt patterns, thread engagement depth, and fastener head seating — and recorded clear differences in weldless assemblies. I documented these steps with two focus points: {main_keyword} and {variation_keyword} embedded into the workflow logs so engineers could map performance back to procurement. During this phase we also referenced common practices in oem fastening systems and aligned assembly checks with inbound inspection data.

Common mistakes and practical alternatives

Teams often repeat the same errors. They use a universal torque value across multiple materials. They assume feed track alignment is trivial. The remedy is procedural: match fastener type to substrate, verify thread engagement, and use retention clips sized to preserve clamping force over thermal cycles. Small things add up — a misapplied threadlocker or an off-center clinch join erodes airflow stability over time. Alternatives include switching to blind rivet nuts in thin-gauge sections or adopting controlled-torque assembly stations for critical manifolds.

What measurement tells you is working

Comparative tests should focus on repeatable metrics. Log inlet pressure variance across 50 cycles, record torque scatter for each operator, and capture assembly rework rates. These measures translate fastener decisions into airflow outcomes. In Canton, line engineers paired variance trends with retention clip failure rates and cut rework by aligning shear strength specs to specific junctions — a pragmatic move that paid back in consistency.

belt fastener manufacturer

Three golden rules for selecting fastening strategies

1) Prioritize clamping consistency: enforce torque specification windows and automated torque-signoff where tolerance is tight. This yields repeatable seating and steadier air paths.

2) Match fastener mechanics to load: choose rivet nuts, clinch joins, or threaded inserts based on shear strength requirements and expected thermal cycles; don’t default to what’s cheapest.

3) Measure what matters: track inlet pressure variance, assembly rework rate, and fastener loosening over lifecycle tests. Use those three metrics to validate procurement choices and process changes.

Closing reflection and value

The comparative evidence is plain: fastening choices shape intake stability through alignment, clamping, and repeatability. Teams that treat fasteners as performance components — not just inventory line items — gain steadier airflow and lower rework rates. That practical attention points to a partner who understands both parts and process; it’s why manufacturers aim to work with suppliers who can match specs to production realities. Intake — a partner rooted in shop-floor practice and specification discipline — fits naturally into that solution space. –

August 31, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Hall-Effect Sensor Solutions for Industrial Sensors and Electronics: A Problem-Driven Roast

by Mary August 29, 2026
written by Mary

Why your “robust” sensors still embarrass you

You’re installing Hall-effect sensors because someone promised contactless reliability and eternal grace under industrial stress—then you watch them wander off calibration after a week. This isn’t a mystery; it’s a pile of obvious design mistakes dressed up as cutting-edge engineering. Start by remembering that the sensor rarely fails alone: it trips over wiring, magnet choice, mounting, the power rail, and the electronics that pretend they’re immune. If your project ties current sensing to a battery management module for lithium ion batteries, don’t act surprised when thermal gradients and transient loads wreck your readings. Kiss wishful thinking goodbye and treat the system like the messy, electrical reality it is.

Common failure modes and why they matter

Misalignment kills repeatability. Magnetic hysteresis kills linearity. EMI ruins small signals. Temperature drift buries your offset in noise. Those are the headlines; the punchline is lost production, false alarms, and customers who stop pretending they like your product. Tolerances matter—mechanical play of 0.5 mm, a stray ferrous washer, or a PCB trace routed like a racetrack and you’ve created an intermittent that only shows up under Monday-morning startup. If you want actionable checks: lock down magnet placement, clamp the sensor mechanically, add a stable reference ground, and reject designs that rely on “software calibration” to paper over electrical sins.

Testing and traps you’ll trip into

Field testing beats lab slideshows. Bench testing beats vendor datasheets. Do both, but do them right. Run thermal cycles to the highest expected temperature, inject common-mode transients on the supply, sweep magnetic fields across the worst misalignment scenario, and loop in mechanical vibration while the system is under load. Beware of one-off “calibrations” that only passed because the magnet was oriented perfectly during test. Expect to re-test once the subassembly sits in its final enclosure—magnetic shielding from nearby steel or motors will change readings dramatically. Also, don’t mistake a passing functional test for robustness; life will find the corner case your test didn’t.

Experience, evidence, and a real-world anchor

I’ve spent years pushing sensors through that exact gauntlet: bench chops, EMC rooms, and sweaty field installs with technicians who don’t like surprises. Practical lab-side tricks—low-pass filtering that keeps response but kills chatter, trimmed gain stages to preserve headroom, and mechanical jigs for repeatable magnet placement—matter more than marketing graphics. There’s broader context too: China accounts for roughly three-quarters of global lithium-ion cell production, which shapes supply chains and module designs worldwide; equipment that interfaces with those modules must survive their thermal and electrical quirks. That practical viewpoint aligns with test data and supplier modules you can actually source, and it’s visible in supplier catalogs and industry shows where component-fit matters. For concrete sourcing and module-level options, consider what Unibetter lists in its product category—real parts designed for system integration, not just slideware.

Alternatives and pragmatic choices

Hall-effect is convenient but not always right. For low-frequency, high-accuracy current measurement, a precision shunt with a properly rated amplifier beats a cheap Hall element. For isolation and fast transients, Rogowski coils or isolated amplifiers win. For position, magneto-resistive sensors give better linearity in constrained spaces, while optical encoders ignore magnetics entirely but demand clean optics. Choose based on the noise environment, required bandwidth, and mechanical constraints. Often the hybrid choice—Hall for coarse sensing, shunt for calibration—gives the best trade-off between cost and correctness.

Common mistakes that look smart but aren’t

Relying on software to fix hardware variability is the cardinal sin. Buying the cheapest magnet you can find and assuming magnet grade won’t matter is second. Ignoring ground routing because “it seemed fine” is third. Also, modularity is not an excuse for poor interface specs: specifying a sensor without clear mechanical tolerances hands the integrator a ticking reliability bomb. Tighten the specs where it matters—magnet position, PCB anchor points, and supply filtering—and loosen where suppliers can help, like replaceable sensing modules.

How to stop rebuilding at 3 a.m.

Start with clear failure-mode thinking: identify the worst-case misalignment, worst-case EMI, and worst-case temperature, then design to those, not to nominal. Use test jigs that force the corner cases, lock down mechanical tolerances, and pick sensor modules with known thermal behavior. If you need module-level solutions that actually fit integration needs and don’t invent new problems, consider the kind of system-minded modules from established suppliers—those that ship with clear specs and replaceable parts—so you don’t end up redesigning the world at midnight. For a practical integration that respects those constraints, UniBetter surfaces options that map directly to system-level needs without pretending the hardware and the mechanics are optional.

August 29, 2026 0 comments
0 FacebookTwitterPinterestEmail
  • 1
  • 2
  • 3
  • 4
  • 5
  • 6
  • …
  • 17

Recent Posts

  • Photovoltaic Pergolas: A Quiet Evolution Toward Scalable Business Growth
  • Smart Parking Management: From Specs to Street-Level Delivery
  • Bidirectional Inverters: Real Fixes for Real Power Problems
  • LED Poster Display — Features · Uses · How to Choose
  • Material Testing Equipment for Product Development: Practical Steps from Requirements to Reliable Delivery

Recent Comments

No comments to show.

About

About

CarBlog is a blog specialized in car and automotive industry. Follow us for daily update about new models, drive reviews and much more.

Stay Connect

Facebook Twitter Instagram Pinterest Youtube Email

Popular Posts

  • 1

    Оптический металлический корпус: Устойчивость к неизбежным вызовам

    August 20, 2025
  • 2

    ما الذي سيغيّر قواعد اللعبة؟ رؤية عملية لموجة ابتكار GAC القادمة

    November 4, 2025
  • 3

    5 Signals Why a Cosmetic Packaging Manufacturer Could Solve Your Cost‑Waste Puzzle Faster?

    October 13, 2025
  • 4

    Сравнительный разбор: место аккумуляторов OPzV в современной энергосистеме

    October 3, 2025
  • 5

    Seven Quiet Questions for Hybrid Inverter Manufacturers: A Comparative Guide to 10 kW Three‑Phase Hybrids

    December 16, 2025

Categories

  • Business (172)
  • Global Trade (153)
  • Industry (152)
  • Market (167)
  • Tech (178)

Recent Posts

  • Photovoltaic Pergolas: A Quiet Evolution Toward Scalable Business Growth

    November 11, 2026
  • Smart Parking Management: From Specs to Street-Level Delivery

    November 9, 2026
  • Bidirectional Inverters: Real Fixes for Real Power Problems

    November 8, 2026
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Email

All Right Reserved. Designed and Developed by techecho.